Related Experiment Video
Updated: Feb 3, 2026

Determination of the Excitation and Coupling Rates Between Light Emitters and Surface Plasmon Polaritons
Published on: July 21, 2018
Microstructure of High-Performance Aluminum Alloy Surface Processed by the Single-Excitation Same-Frequency
Chongyang Zhao1, Xiaobo Wang2, Bo Zhao3
1School of Mechanical and Power Engineering, Henan Polytechnic University, Jiaozuo 454000, China. zhaocy@hpu.edu.cn.

Abstract:
The high performance of parts is determined by the microstructure of the machined surface to some extent. Different processing methods have been used to construct different microstructures on machined surfaces; the effective improvement of the serviceability of parts has been the focus of research in the field of precision and ultra-precision machining. In the presented work, a microscratch was formed on the machined surface in ultrasonic assisted machining, and the surface microstructure of high-performance aluminum alloy processed by single-excitation rotational longitudinal⁻torsional coupled ultrasonic vibration (LTCUV) milling was investigated. First, the motion paths model of the cutting edge in the LTCUV milling were established; then, the single-excitation LTCUV milling system has been set up, and the acoustic performance of the LTCUV system was examined. The surface microstructure of aluminum alloy was processed by different machining techniques, and the effect of processing parameters on the surface microstructure and performance were investigated by the orthogonal design of experiment (DOE). The surface roughness was found to be proportional to the ultrasonic cutting speed and feeding rate. The surface roughness was mainly controlled by the ultrasonic amplitude, and the optimal surface quality corresponded to the ultrasonic amplitude of 4 μm. The cutting speed contributes greatly to the surface roughness. The water contact angle of surfaces obtained by ultrasonic processing was larger than that of surfaces achieved by the conventional processing, while the surface water contact angle was negatively related to the ultrasonic amplitude. Once the rotation speed exceeded a critical level, the ultrasonic amplitude exerted a negligible effect on the surface water contact angle. The cutting speed contributes the most to the water contact angle. The friction coefficients of surfaces treated by ultrasonic processing were lower than those obtained by conventional processing at constant processing parameters, while the friction coefficient was minimized at the ultrasonic amplitude of 4 μm. In the case of grease lubrication friction, the surface wear decreased with the ultrasonic amplitude, indicating the improved wear resistance of the processed surfaces. Similarly, the ultrasonic amplitude has the highest contribution rate to friction and wear.
Related Concept Videos
 01:20
Excitation-Contraction Coupling in Skeletal Muscles
When an action...
 01:16
Torsion of Noncircular Members
 02:20
Longitudinal Research
 01:09
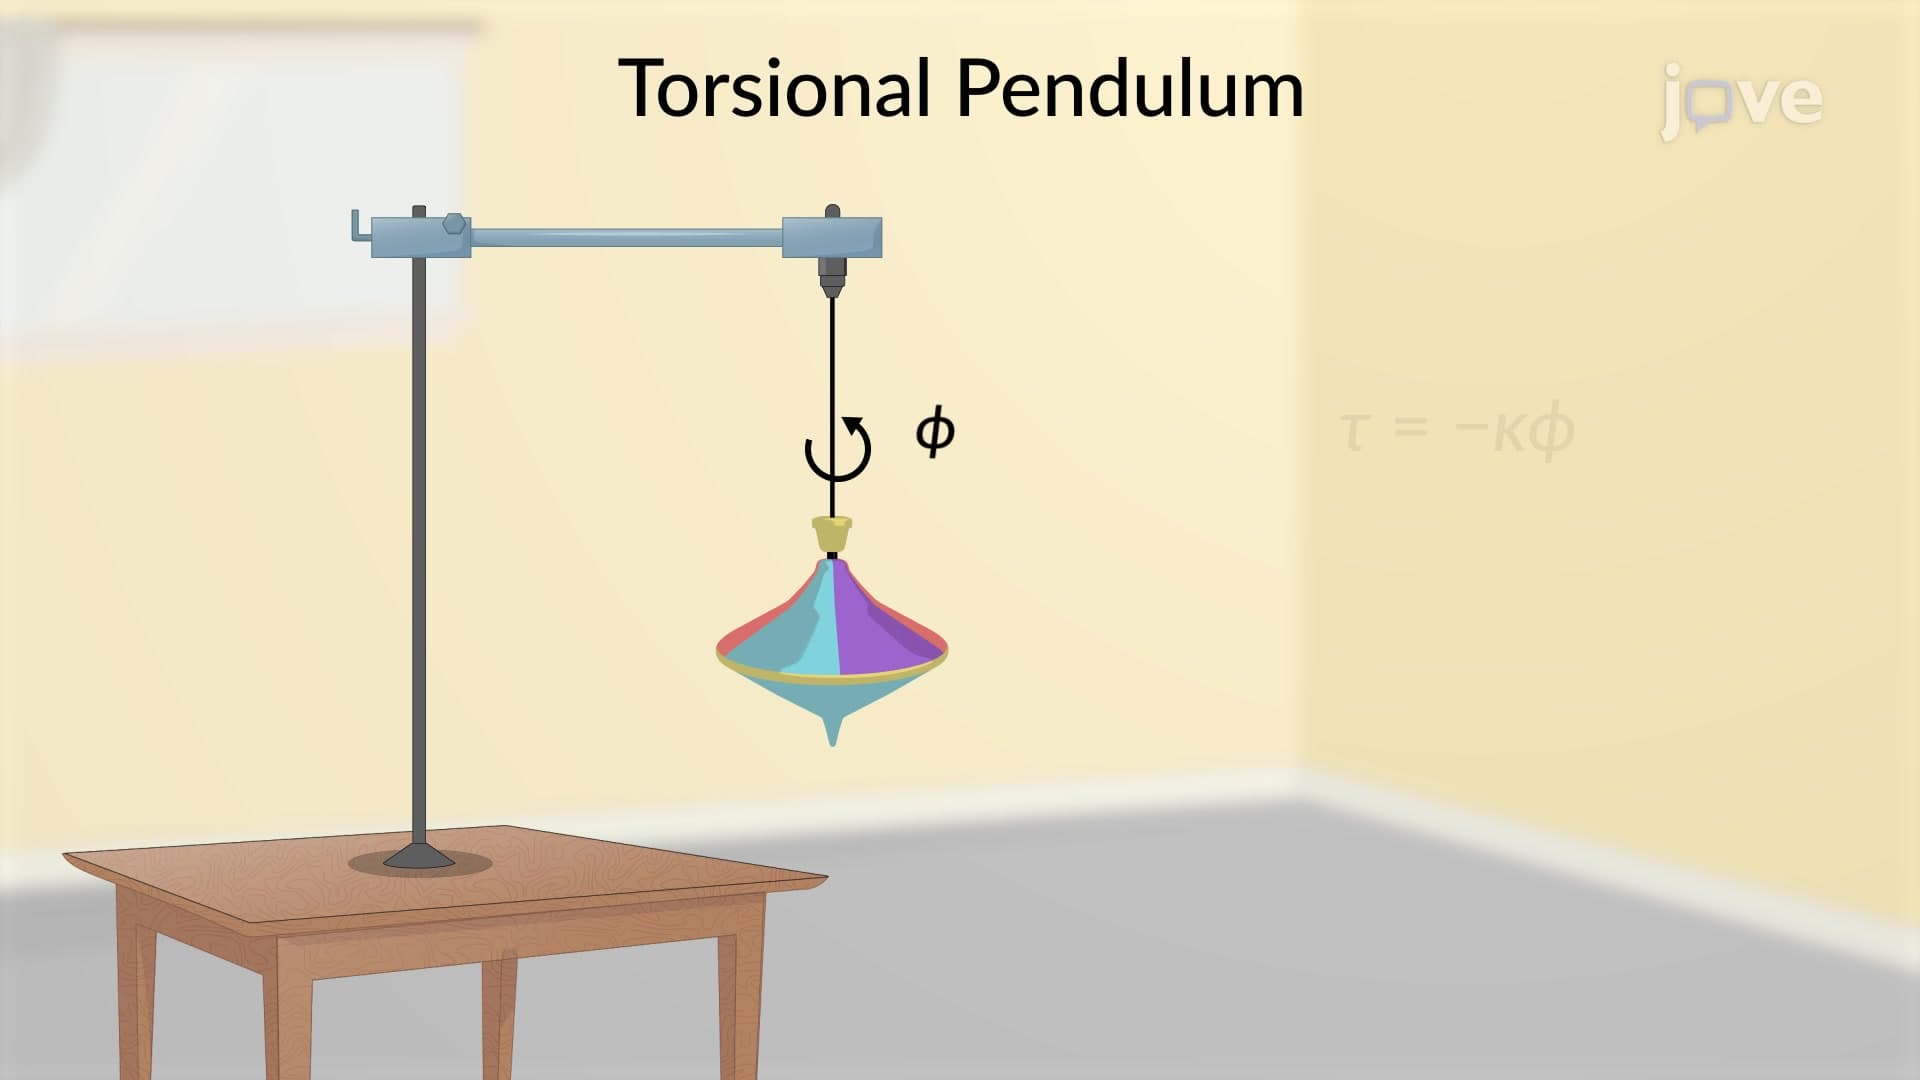
Torsional Pendulum
As long as the rigid body's angular displacement is small, its oscillation can be modeled as a linear angular oscillation. The amplitude of the oscillation is an angle. The role of mass is played...
 01:05
High-Performance Liquid Chromatography: Elution Process
 01:20
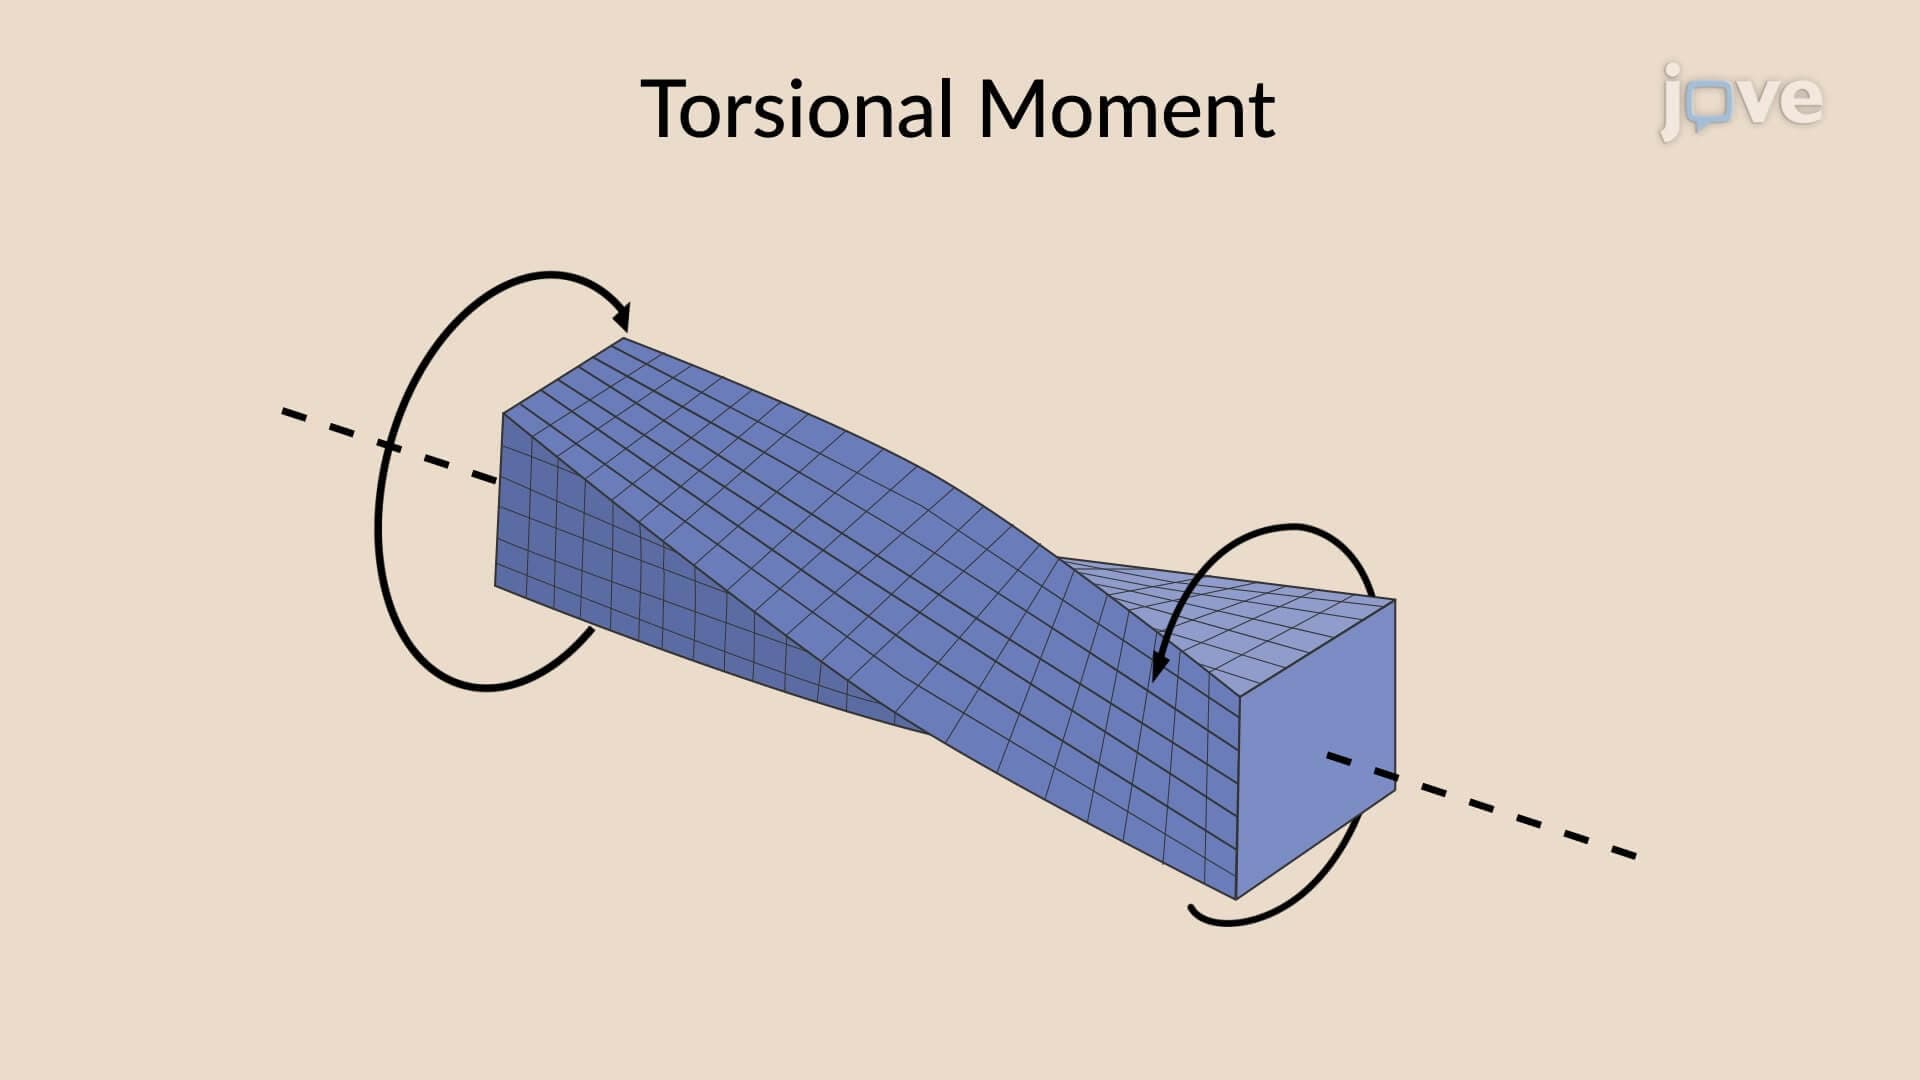
Bending and Torsional Moments
The reaction developed in a structural element when subjected to an external force causes the element to bend. When a structural element bends upwards, it creates compressive normal forces on the top and tensile normal forces on the bottom, resulting in a couple that determines the bending...