Related Experiment Video
Updated: Aug 23, 2025
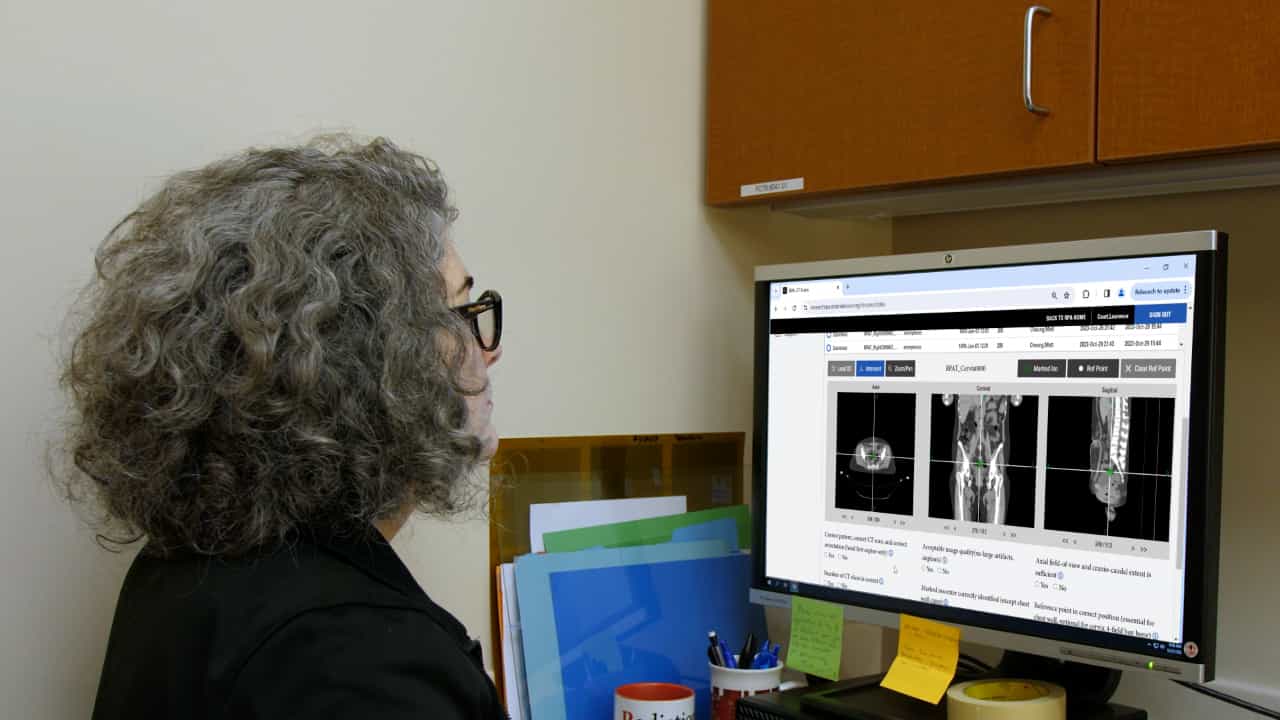

Author Spotlight: Improving Radiation Therapy Access with Radiation Planning Assistant
Published on: October 6, 2023
Statistical process control to monitor use of a web-based autoplanning tool
Hunter Mehrens1,2, Raphael Douglas1, Mary Gronberg1,2
1Department of Radiation Physics, The University of Texas MD Anderson Cancer Center, Houston, Texas, USA.

Purpose:
To investigate the use of statistical process control (SPC) for quality assurance of an integrated web-based autoplanning tool, Radiation Planning Assistant (RPA).
Methods:
Automatically generated plans were downloaded and imported into two treatment planning systems (TPSs), RayStation and Eclipse, in which they were recalculated using fixed monitor units. The recalculated plans were then uploaded back to the RPA, and the mean dose differences for each contour between the original RPA and the TPSs plans were calculated. SPC was used to characterize the RPA plans in terms of two comparisons: RayStation TPS versus RPA and Eclipse TPS versus RPA for three anatomical sites, and variations in the machine parameters dosimetric leaf gap (DLG) and multileaf collimator transmission factor (MLC-TF) for two algorithms (Analytical Anisotropic Algorithm [AAA]) and Acuros in the Eclipse TPS. Overall, SPC was used to monitor the process of the RPA, while clinics would still perform their routine patient-specific QA.
Results:
For RayStation, the average mean percent dose differences across all contours were 0.65% ± 1.05%, -2.09% ± 0.56%, and 0.28% ± 0.98% and average control limit ranges were 1.89% ± 1.32%, 2.16% ± 1.31%, and 2.65% ± 1.89% for the head and neck, cervix, and chest wall, respectively. In contrast, Eclipse's average mean percent dose differences across all contours were -0.62% ± 0.34%, 0.32% ± 0.23%, and -0.91% ± 0.98%, while average control limit ranges were 1.09% ± 0.77%, 3.69% ± 2.67%, 2.73% ± 1.86%, respectively. Averaging all contours and removing outliers, a 0% dose difference corresponded with a DLG value of 0.202 ± 0.019 cm and MLC-TF value of 0.020 ± 0.001 for Acuros and a DLG value of 0.135 ± 0.031 cm and MLC-TF value of 0.015 ± 0.001 for AAA.
Conclusions:
Differences in mean dose and control limits between RPA and two separately commissioned TPSs were determined. With varying control limits and means, SPC provides a flexible and useful process quality assurance tool for monitoring a complex automated system such as the RPA.
More Related Videos
Related Concept Videos
 01:15
Introduction to Statistical Process Control
 01:10
Statgraphics
 01:25
Interpreting Run Charts
 01:05
Quality Control
Quality control helps track data, visualize trends, and identify variations, making it easier to detect deviations that may affect the accuracy of an analysis. One way to do this is by generating a quality control chart, which...
 01:12
Run Charts
 00:58
The X̄ Chart
The x̄ chart, often known as the individual control chart, is a crucial tool in statistical process control. It is designed to monitor process behavior and performance over time and is widely used in various industries to ensure that processes are operating at their optimum capacity and within specified limits.
A x̄ chart is constructed by plotting individual measurements of a quality...