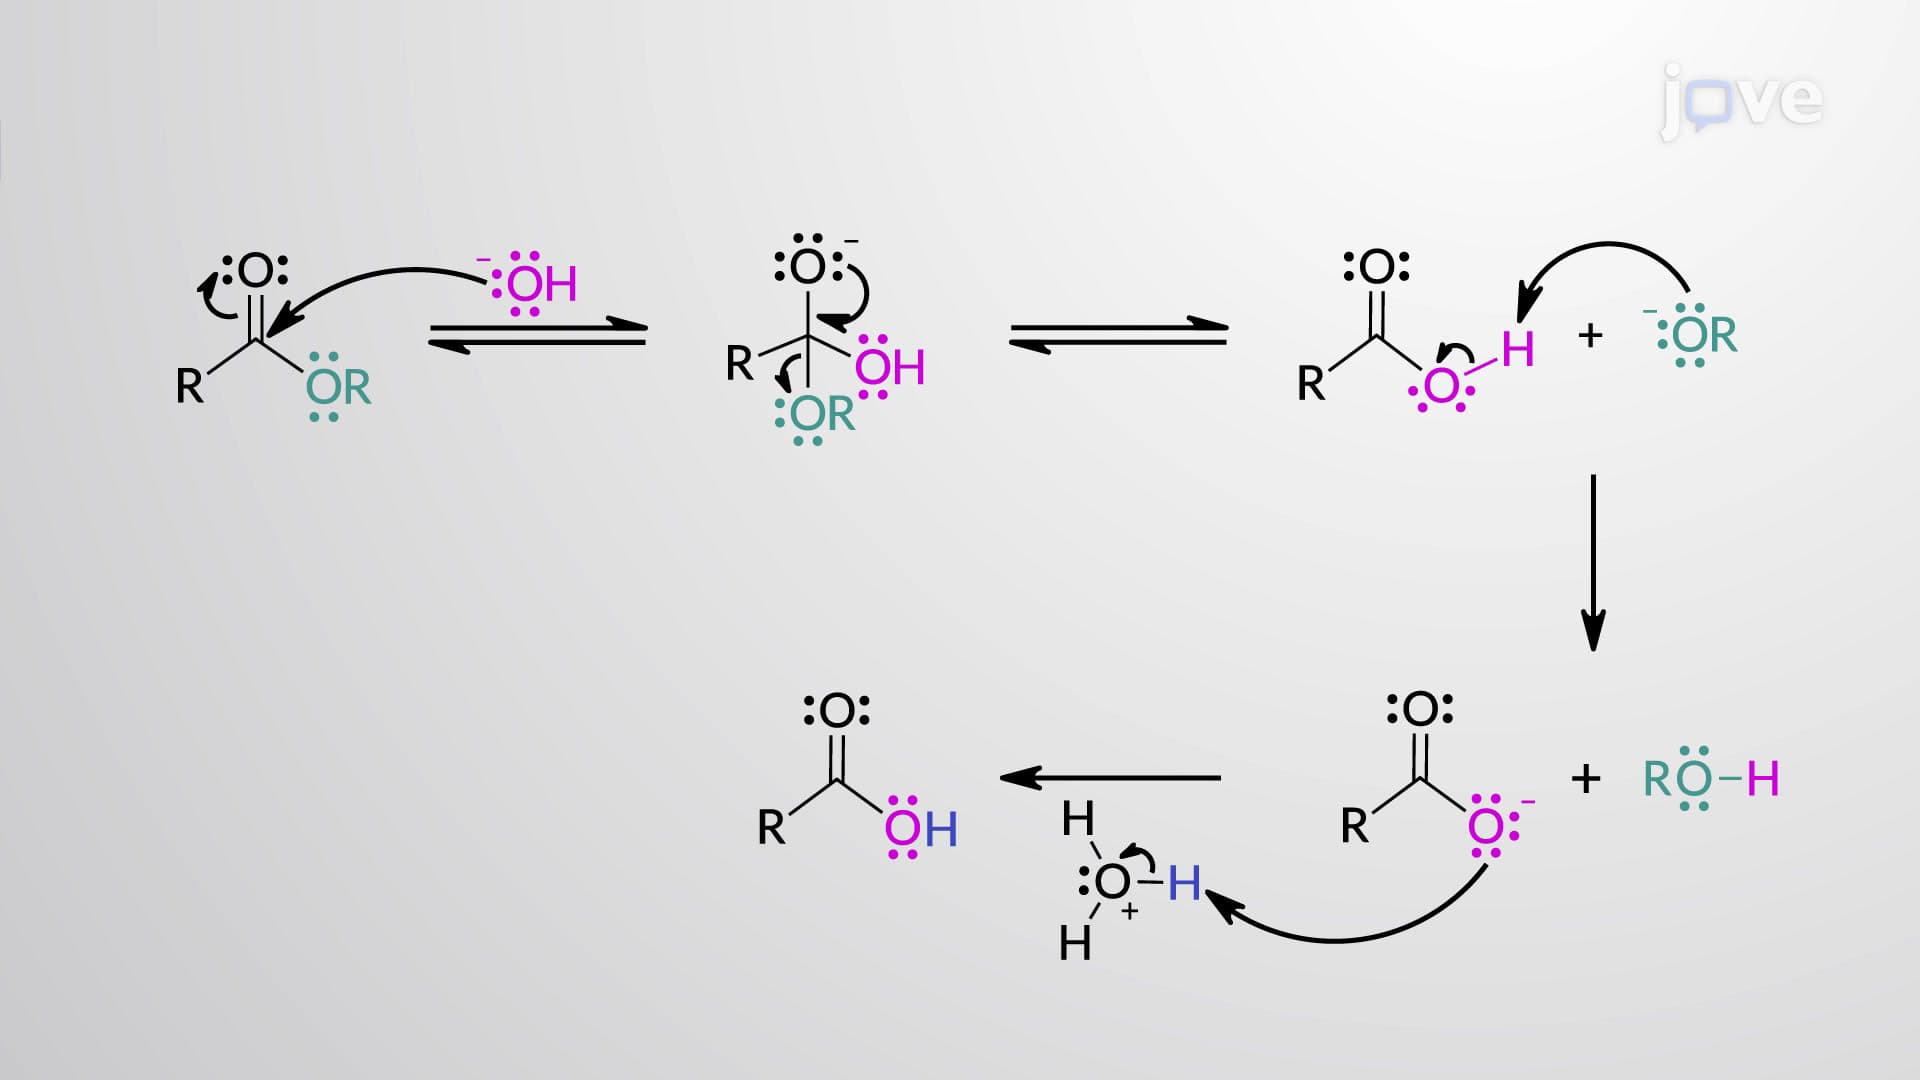
Related Experiment Video
Updated: Jul 23, 2025

Author Spotlight: Employing Green-Chemistry Principles for Safe and Sustainable Synthesis of Biodiesels
Published on: April 19, 2024
Utilizing an ultra-sonication process to optimize a two-step biodiesel production from Karanja oil
Suvik Oza1,2, Harshil Thakar1,2, Pravin Kodgire3,4
1Chemical Engineering Department, Pandit Deendayal Energy University, Gandhinagar, Gujarat, India, 382426.

Abstract:
Currently, biodiesel is produced from non-edible oils, which have various poisonous and un-saponifiable components; therefore, it is harmful and unfit for humans. Biodiesel replaces petro-diesel fuel, which can be used as additives or substitutes for diesel engines. The novelty of the present study is to optimize the process parameters of a two-step (esterification and transesterification) process for biodiesel production using high free fatty acid (FFA) containing Karanja oil (Pongamia pinnata oil), with the ultrasound (US) process intensification (PI) technique, which is carried out for the first time. In the first step, a reduction in the initial FFA concentration of 11.06% was achieved through optimization of the esterification process using response surface methodology (RSM)-supported central composite design (CCD) method in which methanol:oil molar ratio of 6:1 and 60 °C reaction temperature kept as fixed parameter, whereas H2SO4 catalyst loading (0.5-1.5 w/w%) and reaction time (15-45 min.) were varied. The FFA value is reduced to 1.56% under the optimal condition (32.8 min reaction time and 1.14 w/w% of catalyst loading). The second step of optimization of the transesterification of esterified oil was performed by applying RSM supported Box-Behnken design (BBD) method with varying independent parameter ranges such as the molar ratio (A), CH3OK catalyst loading (B), and reaction time (C) with the range of 6:1-9:1 (methanol: oil), 0.5-1.5 w/w%, and 10-30 min., respectively. A biodiesel yield of 98.16% was obtained under optimal conditions of a molar ratio of 7.6:1, catalyst loading of 0.98 w/w%, a reaction time of 20.6 min., and a reaction temperature of 60 °C (constant). Superior optimization results were observed than the conventional stirring method. The biodiesel's estimated characteristics were discovered to be within ASTM criteria and suitable for blending with diesel fuel.
More Related Videos
 09:10
Experimental Protocol for Biodiesel Production with Isolation of Alkenones as Coproducts from Commercial Isochrysis Algal Biomass
Published on: June 24, 2016
 11:33
Laboratory Production of Biofuels and Biochemicals from a Rapeseed Oil through Catalytic Cracking Conversion
Published on: September 2, 2016