Related Experiment Video
Updated: Aug 5, 2026

Production and Analysis of Sporosarcina pasteurii Biocement Bricks Using Custom 3D-Printed Molds for Unconfined Compression Tests
Published on: March 7, 2025
A correction factor for bridging compaction simulator and different roller compactors
Yiwang Guo1, Neha Singh2, Pratap Kasina2
1Department of Pharmaceutics, College of Pharmacy, University of Minnesota, 308 Harvard St. S.E. Minneapolis, MN 55455, United States.

Abstract:
Roller compaction (RC) is an important dry granulation technique. Since pilot and commercial scale roller compactors, which operate continuously on a large scale, usually require kilograms of material per run, formulation and process development directly on such roller compactors is not practical. In contrast, a compaction simulator (CS) can produce ribblets, also known as "slugs", using only a few grams of material with sinusoidal displacement profile replicating the motion of a specific point on the roll surface. Thus, it is possible to develop RC formulation and process in laboratory using a CS-based material-sparing approach. However, because of the inherently different configurations for applying pressure between die compression and roll compression, translating uniaxial pressure from CS experiments to roll pressure during RC is often unreliable, leading to significant uncertainties in the critical quality attributes of ribbons, such as ribbon solid fraction (or porosity) and mechanical strength. The objective of this study was to identify a correction factor (Kp = uniaxial die compression pressure/roll pressure), by correlating the compressibility profiles from CS and a roller compactor of interest, to enable more reliable process translation from CS to roller compactor. In this study, a Kp value of 0.5 was determined for Alexanderwerk WP120 and validated for Gerteis Mini-Pactor and Bepex Pharmapactor. This value may serve as a starting point for translating the optimal compaction pressure identified based on CS investigation to common roller compactors, requiring only minor adjustments to attain optimal RC process parameters (i.e., roll force and roll gap) for a chosen roller compactor.
Related Concept Videos
 01:22
Compacting Factor test
The procedure begins by placing concrete into the upper hopper without any compaction. Once filled, the bottom door of this hopper is opened,...
 01:24
Factors Affecting Workability
 01:20
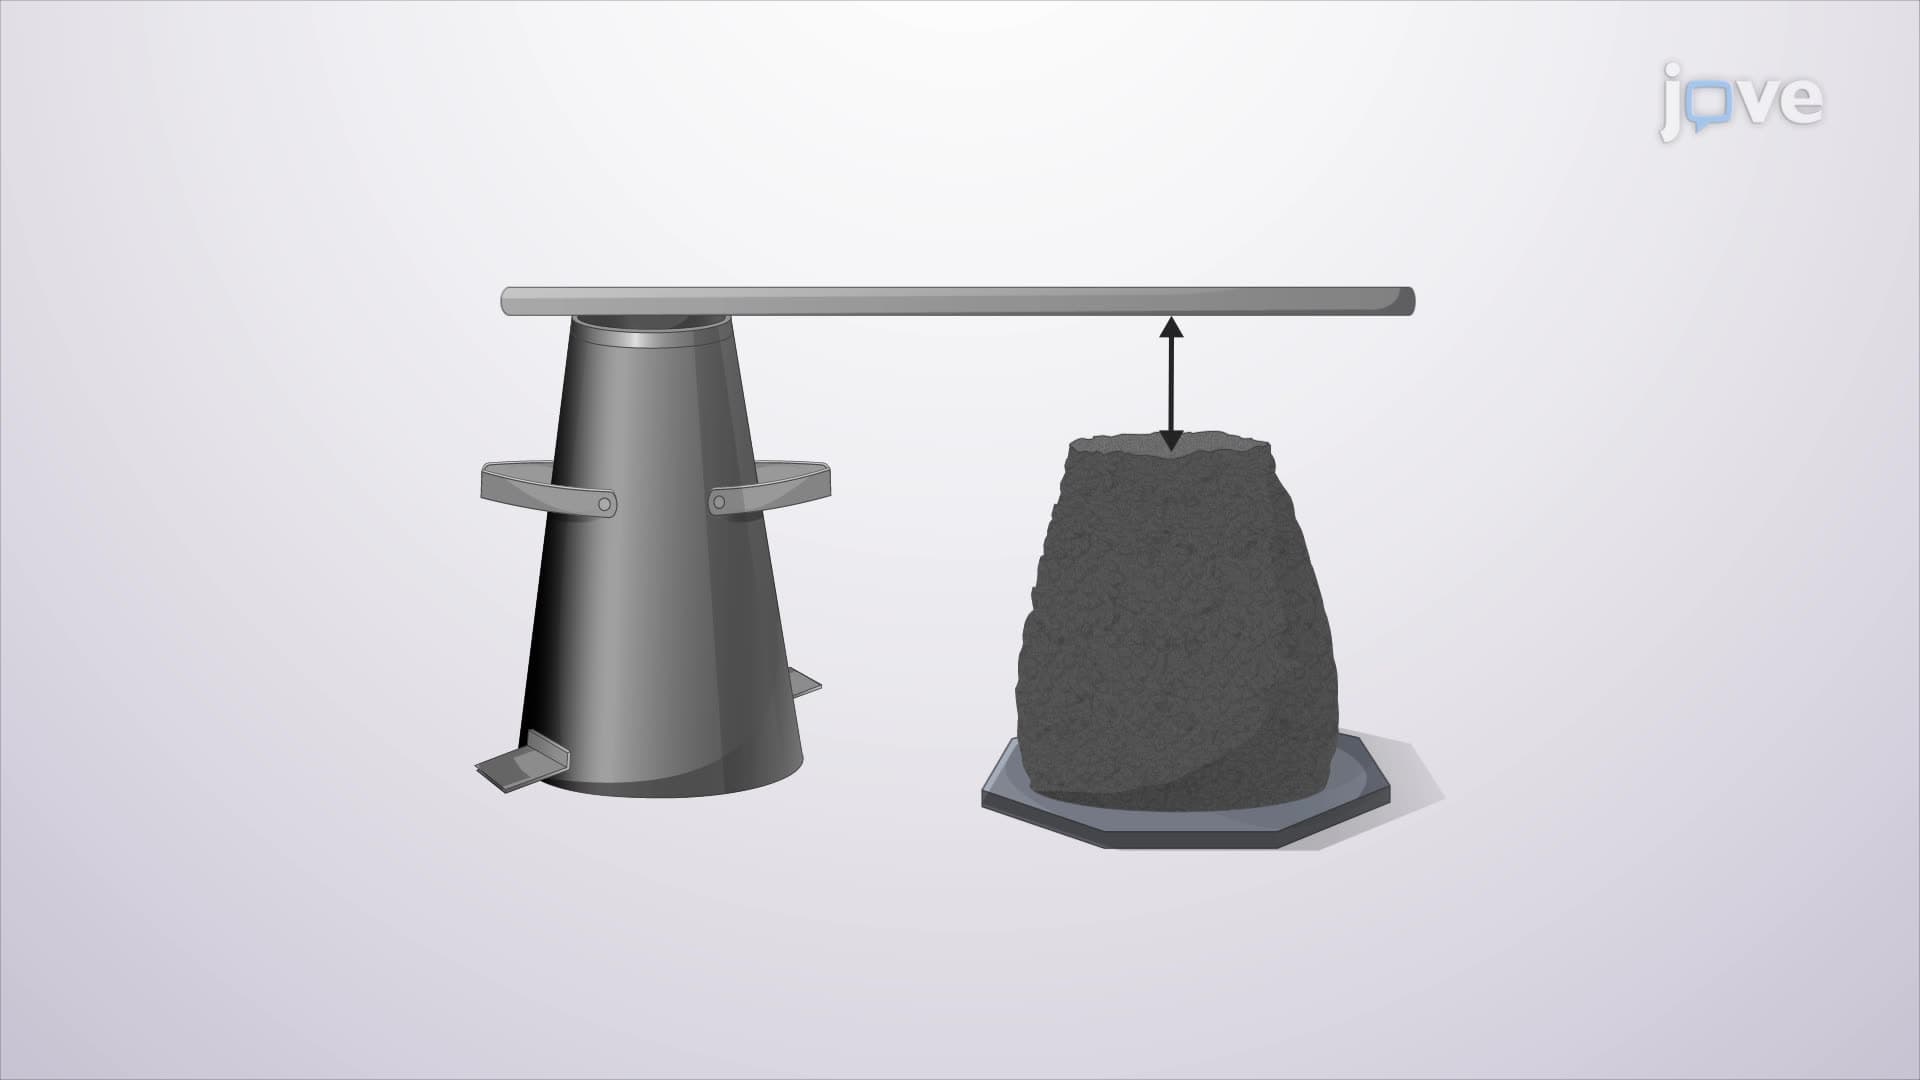
Slump Test
Concrete is poured into the mold in three layers to conduct the test. Each layer is compacted 25 times with a steel tamping rod, which has a five-eighths-inch diameter and a rounded end, to ensure even distribution and eliminate...
 01:22
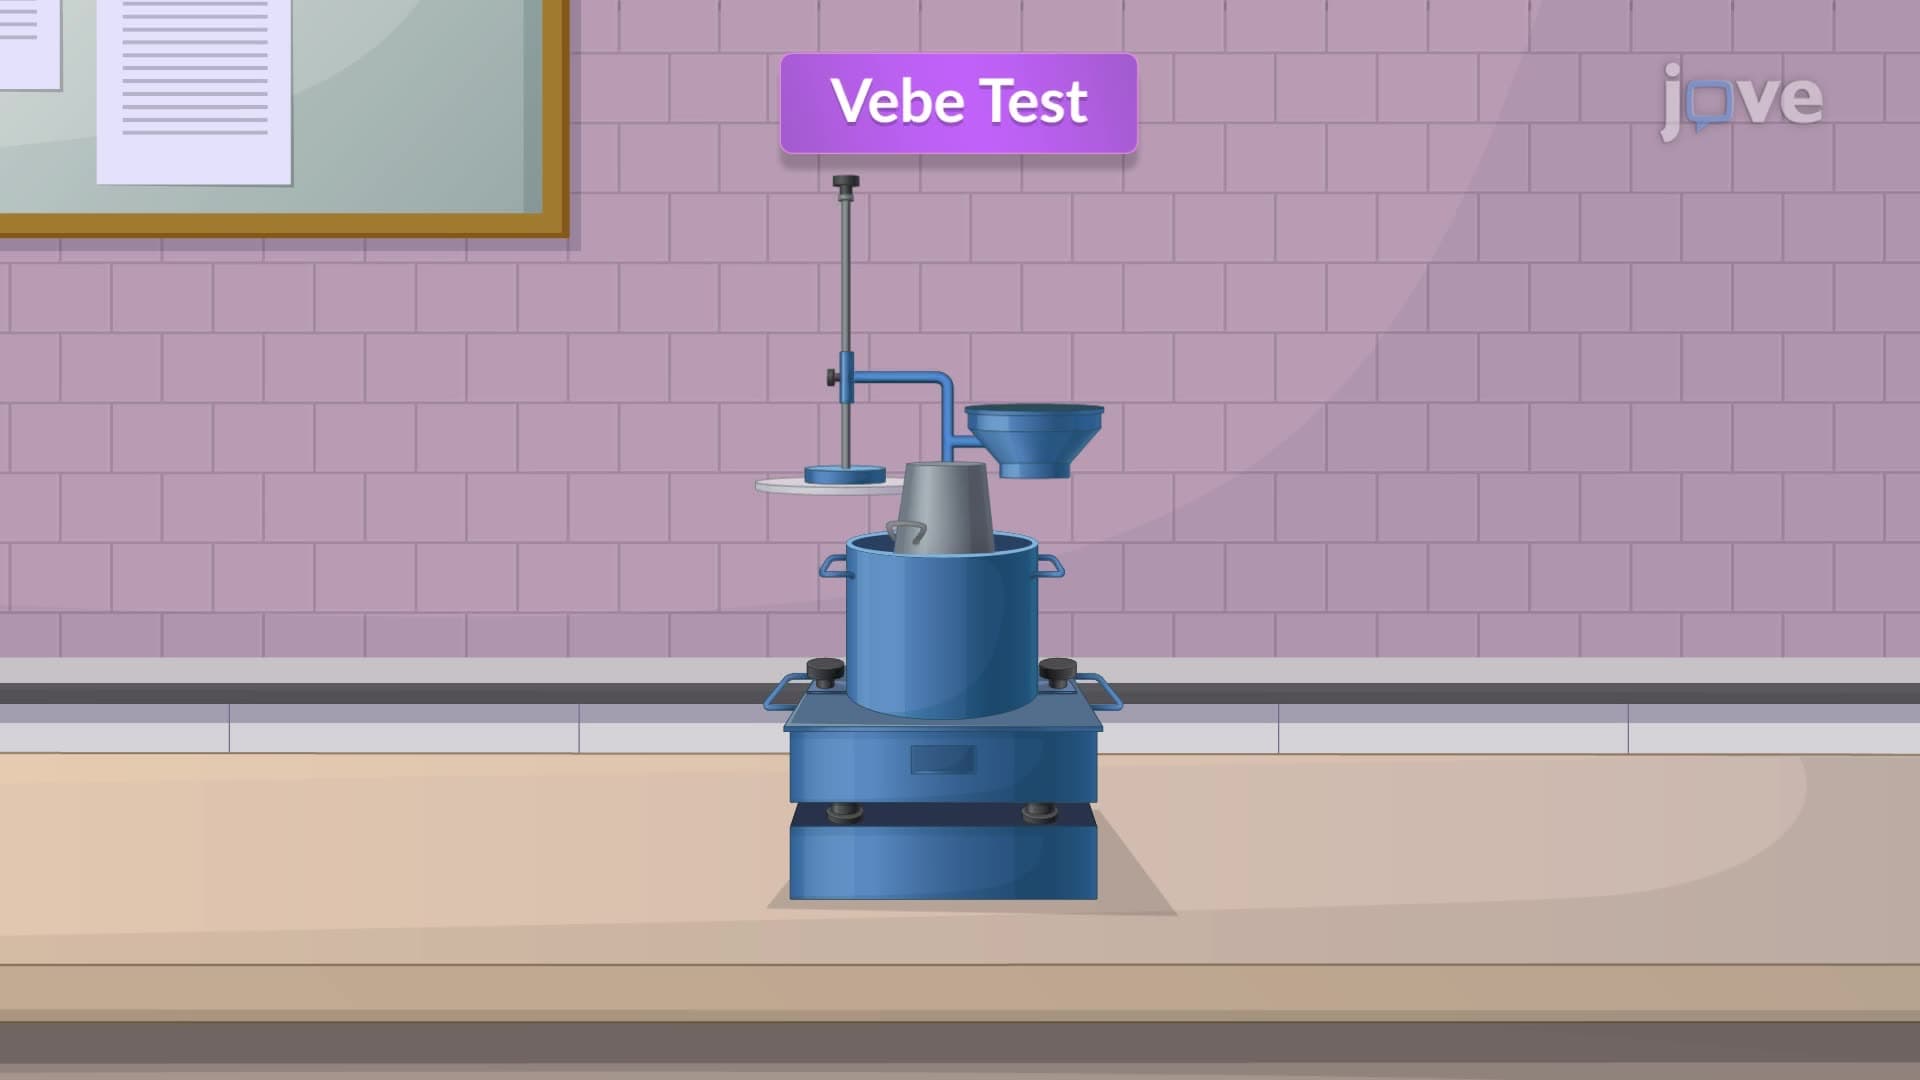
Vebe Test
To conduct the test, concrete is placed into the slump cone. The concrete is filled in layers and...
 01:15
Distance Corrections
 01:17
Rolling Resistance: Problem Solving