Composition-controlled graphene-ZnO-SiC-reinforced aluminum matrix composites: mechanical ranking and minimum quantity lubrication-assisted turning optimization
Related Experiment Video
Updated: Nov 4, 2026
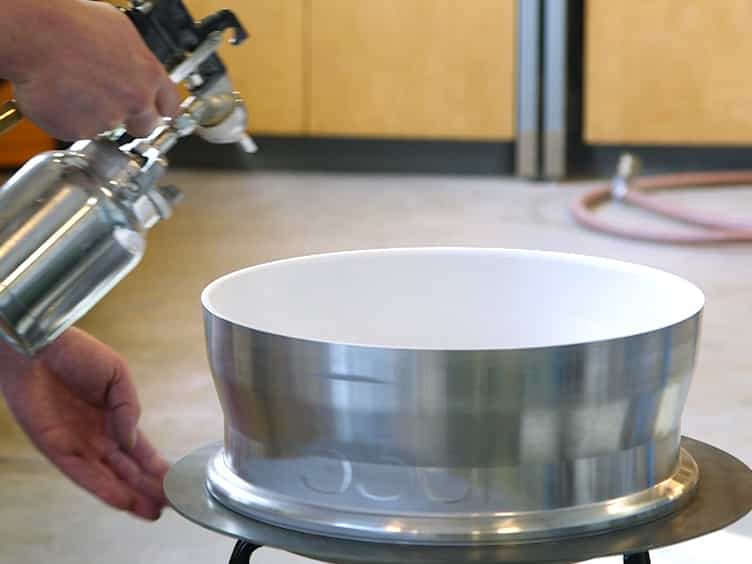
Experimental Procedure for Warm Spinning of Cast Aluminum Components
Published on: February 1, 2017
Md Sazzad Hossain Ador1, Md Mahraj Uddin2, Md Zillur Rahman3
1Department of Industrial and Production Engineering, Ahsanullah University of Science and Technology Dhaka 1208 Bangladesh.

Abstract:
Lightweight aluminum metal matrix composites that combine high mechanical performance with reliable machinability are essential for advanced aerospace, automotive, and precision manufacturing applications. However, simultaneously optimizing strength, damage tolerance, surface integrity, tool wear, and sustainable machining remains challenging, particularly in tri-hybrid systems containing ceramic, carbonaceous, and oxide reinforcements. This study develops composition-controlled graphene-zinc oxide-silicon carbide (Gr-ZnO-SiC)-reinforced aluminum metal matrix composites (Al-MMCs) through a multi-stage stir-casting route, with the Al matrix fixed at 90 wt% and the total reinforcement content maintained at 10 wt%. The internal reinforcement fraction was systematically varied by increasing Gr and ZnO from 1 to 4 wt% each while reducing SiC from 8 to 2 wt%, enabling the identification of a mechanically balanced composition rather than a single-property optimum. Among the fabricated composites, the C3 composition containing 2 wt% Gr, 2 wt% ZnO, and 6 wt% SiC showed the best overall response, achieving a tensile strength of 201.5 MPa, flexural strength of 283.3 MPa, impact strength of 43.3 kJ m-2, and hardness of 69.3 HV. Independent TOPSIS and PCA rankings confirmed C3 as the optimum composition, with a closeness coefficient of 0.967 and a PC1 score of 2.133. FESEM and fractographic analyses revealed a compact microstructure with no large interfacial gaps and a mixed ductile-quasi-cleavage fracture response, indicating effective load transfer, crack deflection, and resistance to localized damage. The optimized C3 composite was subsequently evaluated under dry and minimum-quantity lubrication turning conditions. Relative to dry machining, MQL reduced surface roughness by 43.31%, cutting force by 24.19%, cutting temperature by 8.62%, and chip reduction coefficient by 3.62%, while limiting flank wear from 0.31 to 0.21 mm after 30 min of cutting. Response surface models showed high predictive reliability with no significant lack of fit, and multi-response optimization identified stable MQL-assisted machining conditions of 150 m min-1 cutting speed, 0.16 mm per rev feed rate, and 1.0 mm depth of cut, yielding R a = 1.468 µm, F c = 137.604 N, ξ = 1.702, T = 284.275 °C, and a desirability of 0.897. These findings establish a composition-processing-machining framework for developing damage-tolerant Al-MMCs with balanced structural performance and sustainable machinability.