
一个新的贝叶斯马克斯-EWMA控制图,用于联合监测工艺平均值和方差:对硬烤工艺的应用
Javed Iqbal1, Muhammad Noor-Ul-Amin1, Imad Khan2
1COMSATS University Islamabad, Lahore Campus, Islamabad, Pakistan.
Scientific reports
|December 1, 2023

概括
一个新的贝叶斯马克斯-EWMA控制图有效地监测过程平均值和方程. 这种增强的统计过程控制方法在检测转移以提高制造质量方面表现出卓越的灵敏度.
科学领域:
- 统计过程控制 统计过程控制
- 质量工程 质量工程
- 贝叶斯统计学贝叶斯统计学
背景情况:
- 传统的控制图表往往难以同时有效地监测过程平均值和方差.
- 现有的方法可能对工艺参数的小或中等变化缺乏灵敏度.
- 在制造业中,需要强大的方法来检测工艺分散的变化,这是至关重要的.
研究的目的:
- 引入一个新的贝叶斯最大指数加权移动平均线 (Max-EWMA) 控制图.
- 使用各种损失函数,同时监控正常分布过程的平均值和方差.
- 评估和比较拟议的贝叶斯马克斯-EWMA图表与现有方法的性能.
主要方法:
- 开发一个包含多种损失函数的贝叶斯式Max-EWMA控制图.
- 使用蒙特卡洛模拟计算和分析运行长度特征.
- 根据已建立的控制图表,对运行长度性能进行广泛的比较分析.
主要成果:
- 贝叶斯的Max-EWMA控制图表在检测平均值和方差的变化方面表现出强的整体性能.
- 拟议的图表显示了对检测不同大小的变化具有更高的灵敏度.
- 与现有的控制图表相比,模拟结果证实了优越的运行长度性能.
结论:
- 贝叶斯的Max-EWMA控制图为监测过程平均值和方程提供了更敏感和更有效的方法.
- 在半导体制造 (硬工艺) 中的实际应用凸显了其在现实世界中的有效性.
- 拟议的控制图可靠地检测失控信号,增强质量控制.
相关概念视频
 01:13
Interpreting X̄ Charts
67
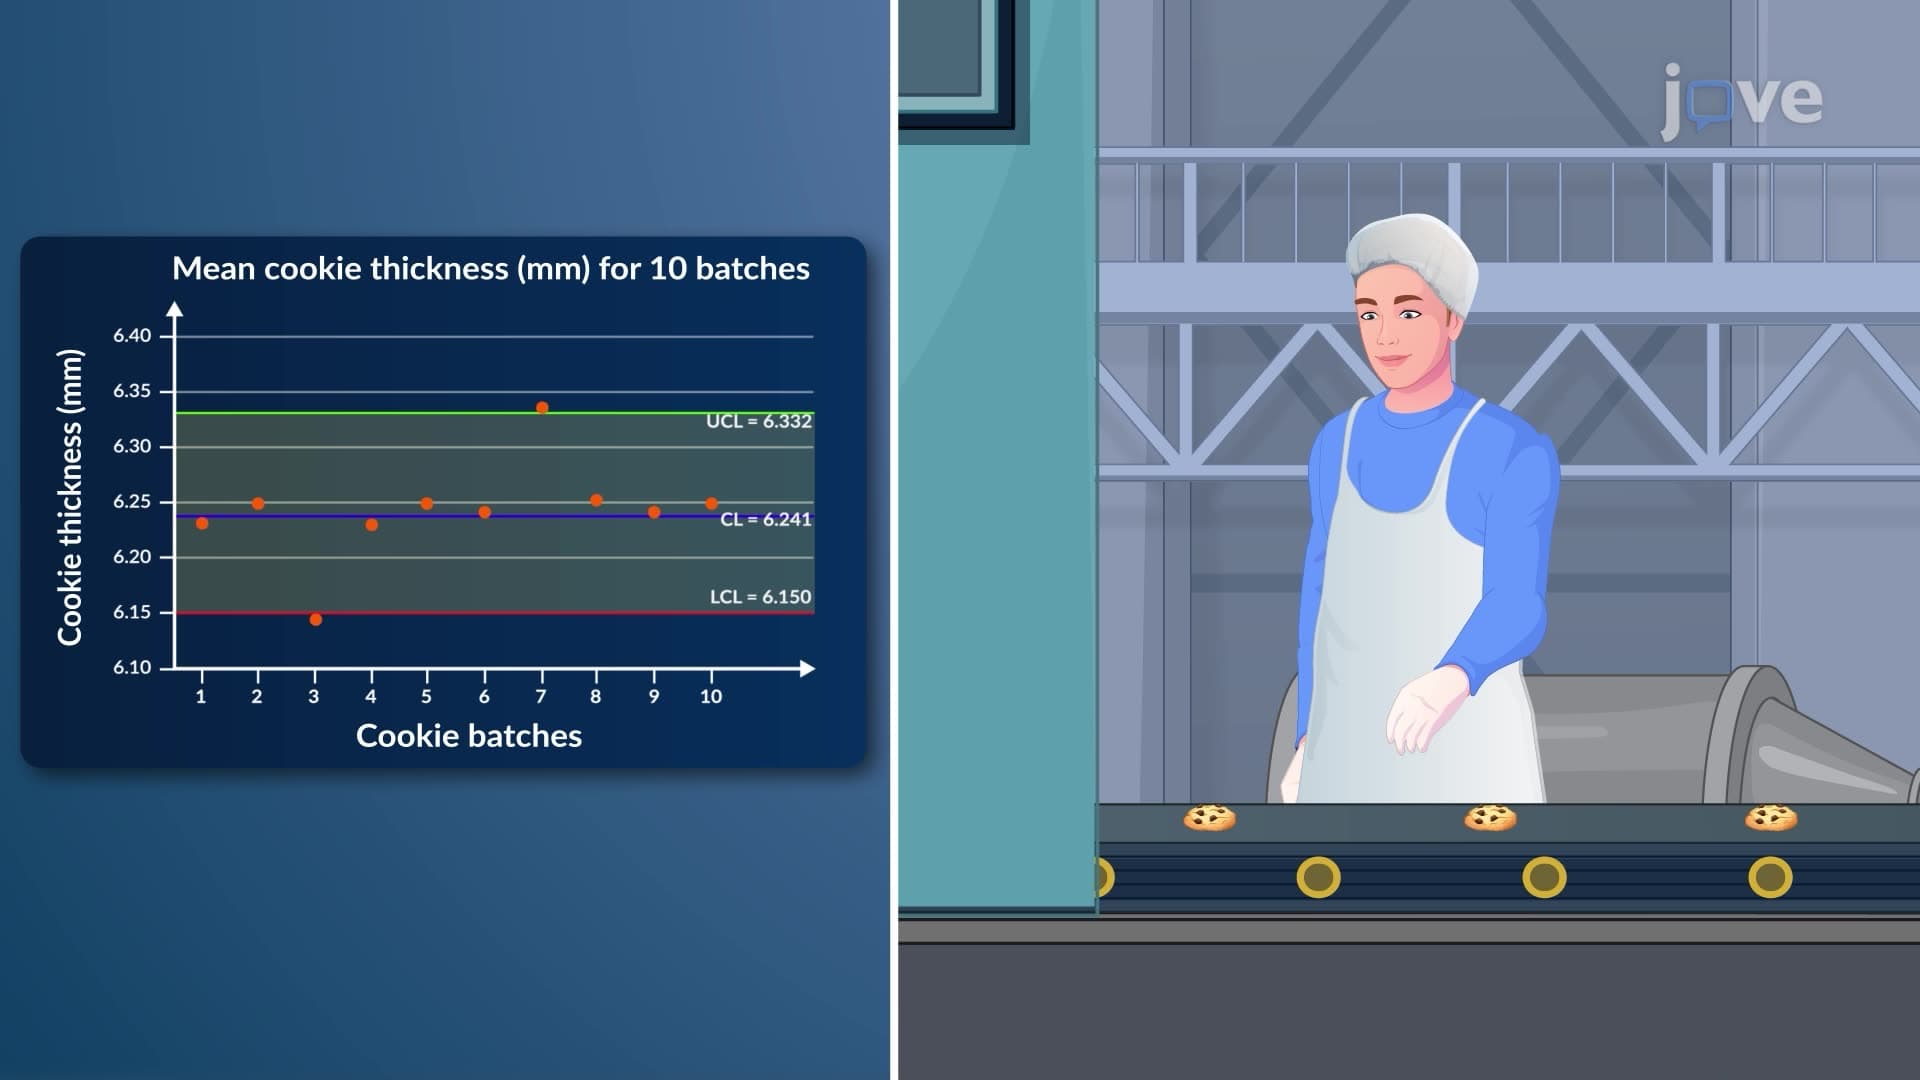
Interpreting x̄ charts, a type of control chart used in statistical process control helps monitor the variation in processes over time. The x̄ chart is based on the sample mean and allows for monitoring variations in the process mean over time. These charts are pivotal for quality assurance in manufacturing and other sectors.
An x̄ chart plots the values of individual measurements over time against control limits calculated from historical data. The central line...
An x̄ chart plots the values of individual measurements over time against control limits calculated from historical data. The central line...
67
 01:22
Interpreting R Charts
67
R chart, or range chart, is a fundamental tool in statistical process control used to monitor the variability within a process. It complements the X-bar (x̄) chart by focusing on the range of the data, rather than individual values, providing a clear picture of the process dispersion over time.
An R chart plots the range of subsets of measurements collected from a process. Each point on the chart represents the range—defined as the difference between the maximum and minimum...
An R chart plots the range of subsets of measurements collected from a process. Each point on the chart represents the range—defined as the difference between the maximum and minimum...
67
 01:02
The R Chart
82
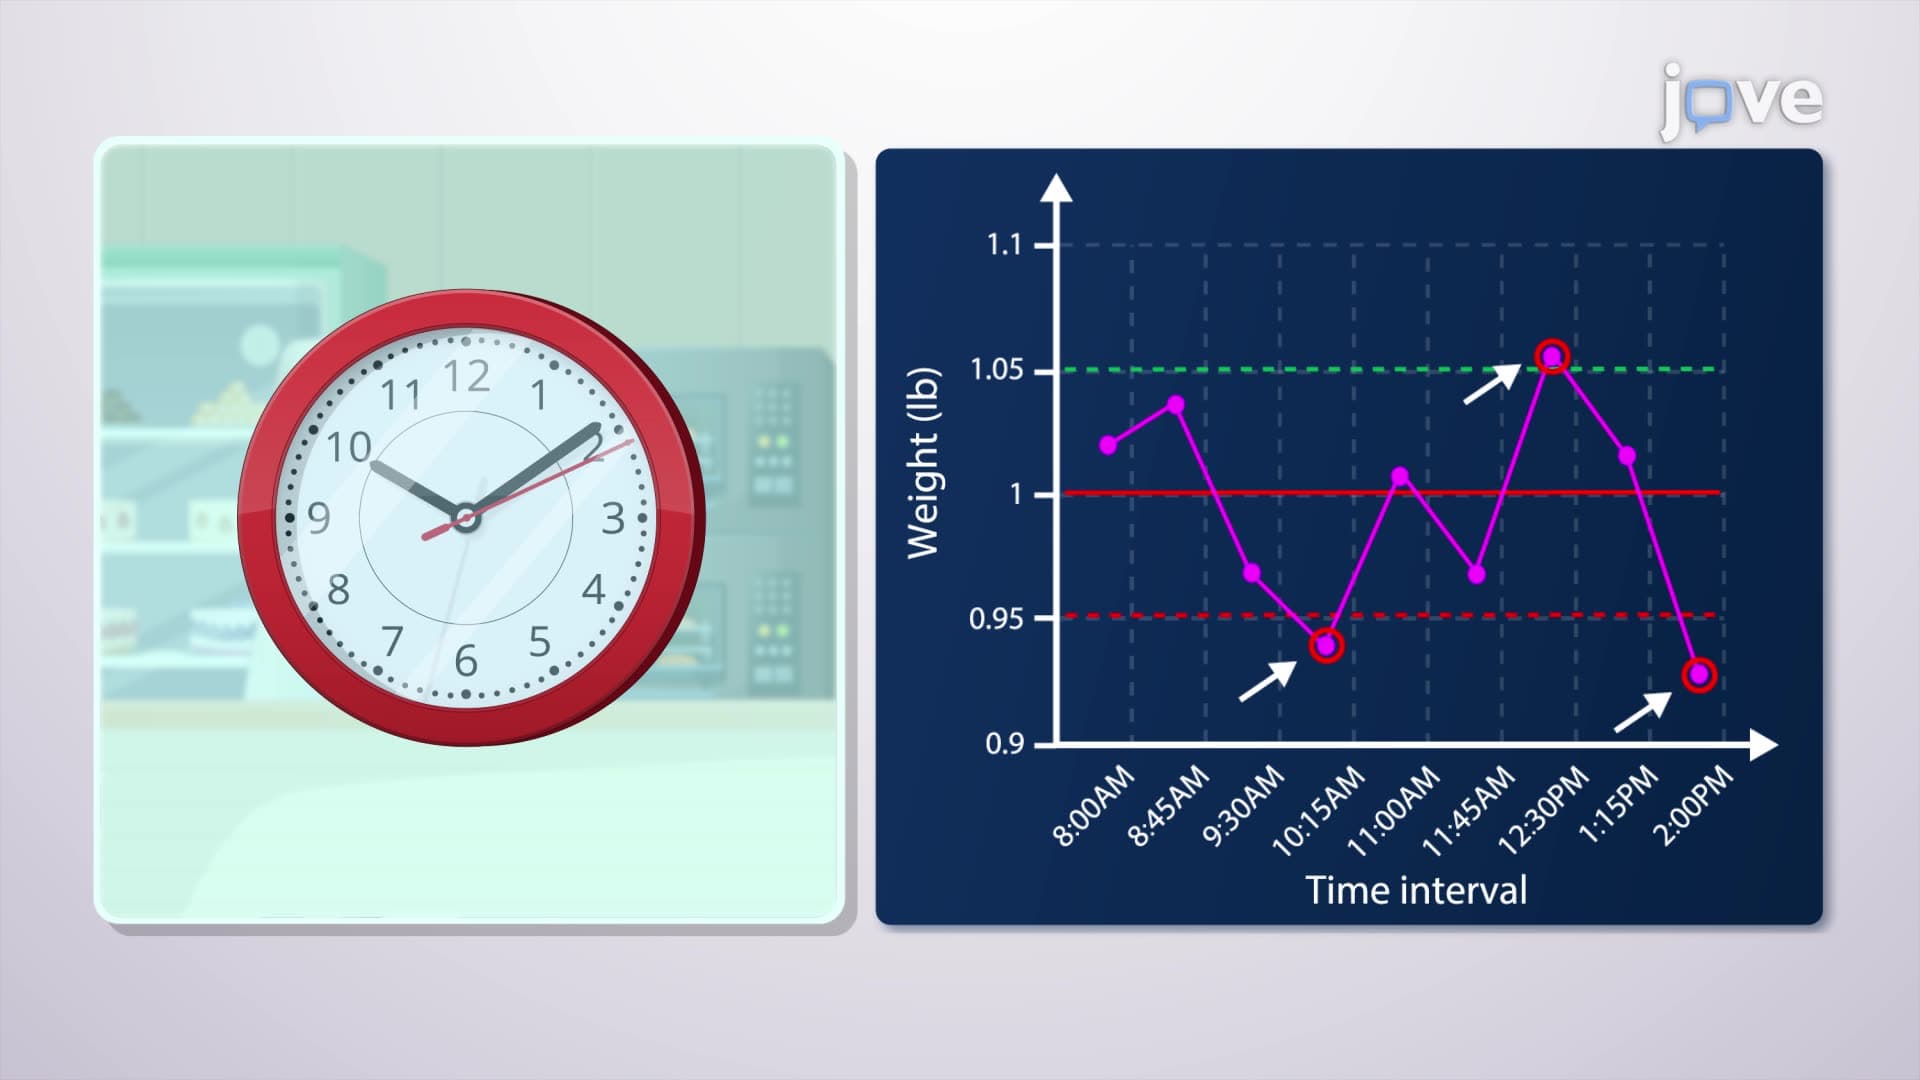
In statistical process control, control charts, particularly R charts, are instrumental in monitoring process variations and identifying non-random patterns that run charts might miss. R charts track the variability within process subgroups, which is crucial when standard deviation use is impractical or unknown process variations exist.
R charts are pivotal for pinpointing shifts in process variability. Stability is indicated when all data points remain within the defined upper and lower...
R charts are pivotal for pinpointing shifts in process variability. Stability is indicated when all data points remain within the defined upper and lower...
82
 00:58
The X̄ Chart
123
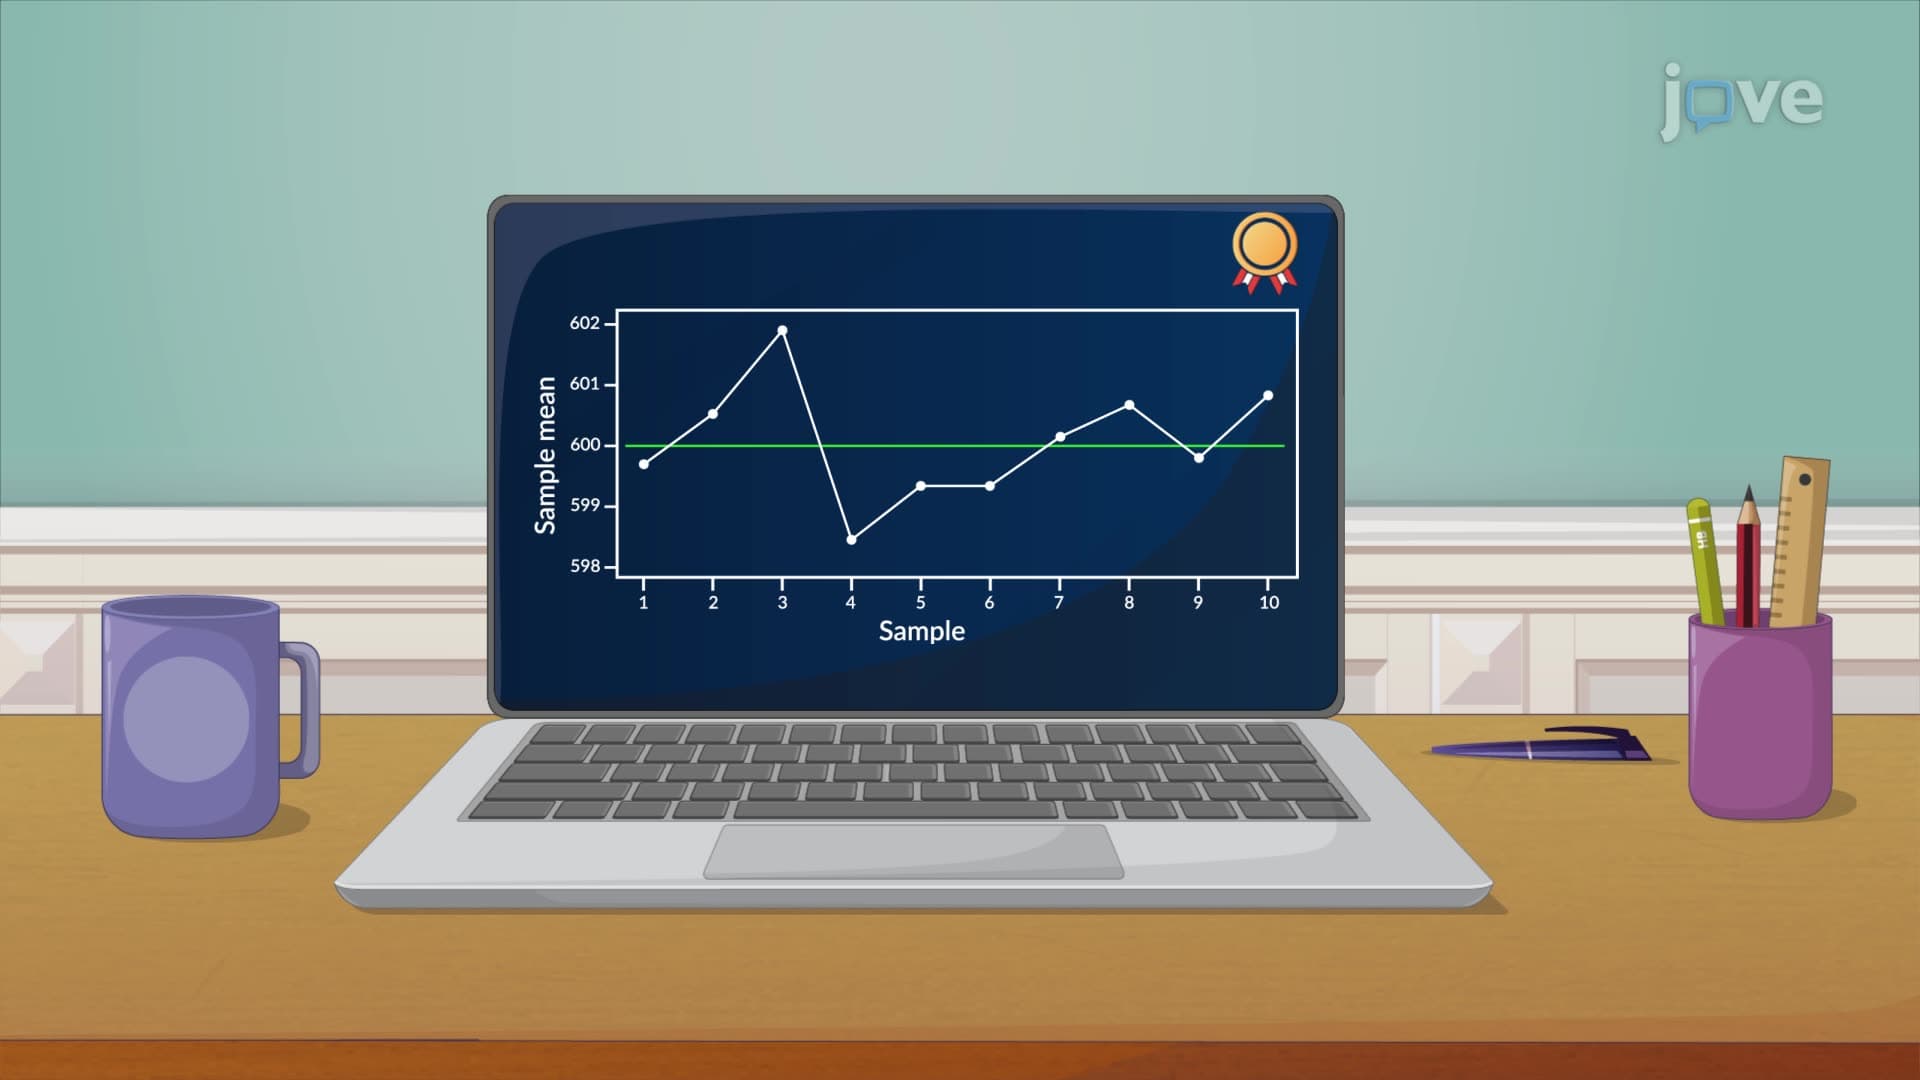
The x̄ chart is a statistical tool for monitoring the means in a process.
The x̄ chart, often known as the individual control chart, is a crucial tool in statistical process control. It is designed to monitor process behavior and performance over time and is widely used in various industries to ensure that processes are operating at their optimum capacity and within specified limits.
A x̄ chart is constructed by plotting individual measurements of a quality...
The x̄ chart, often known as the individual control chart, is a crucial tool in statistical process control. It is designed to monitor process behavior and performance over time and is widely used in various industries to ensure that processes are operating at their optimum capacity and within specified limits.
A x̄ chart is constructed by plotting individual measurements of a quality...
123
 01:15
Introduction to Statistical Process Control
129
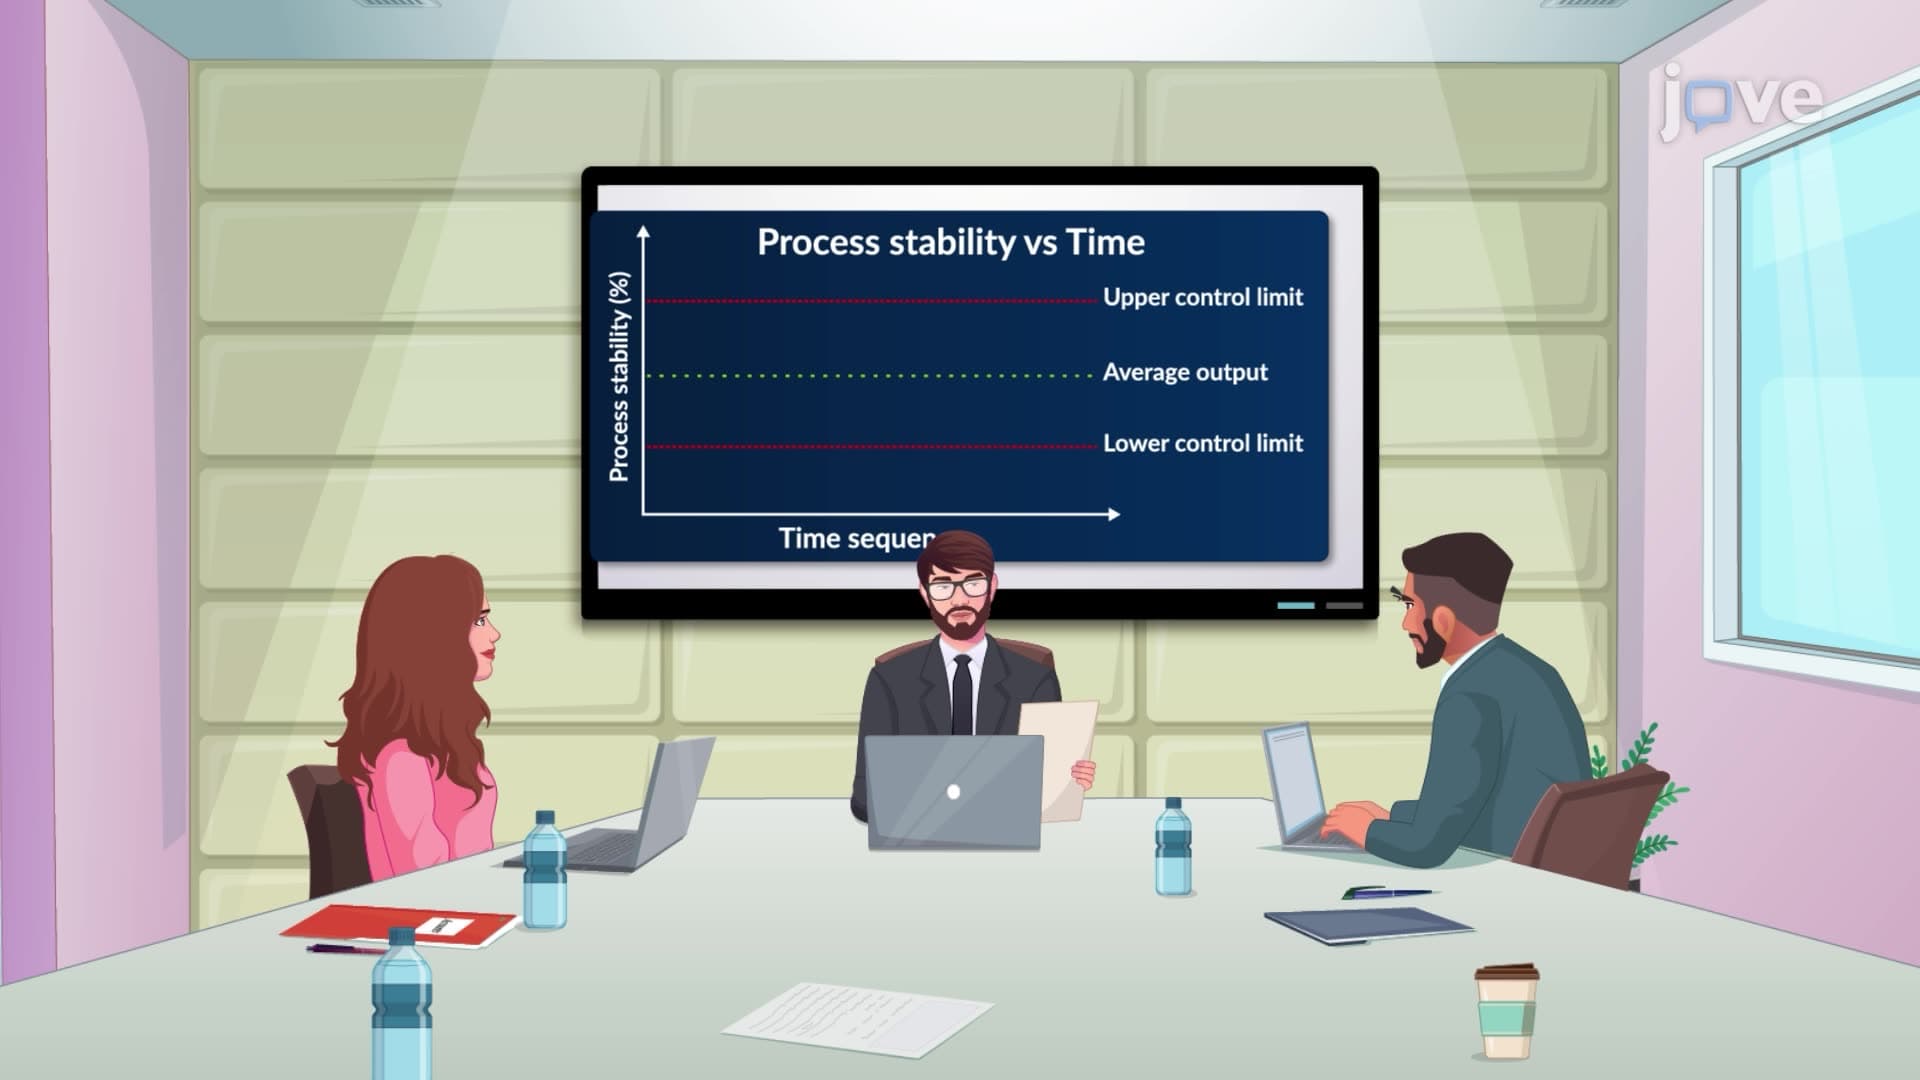
Statistical Process Control (SPC) is a method used to monitor and control quality within processes, particularly in manufacturing and service delivery, by employing statistical methods. SPC aims to distinguish between natural (common cause) variation and variation due to specific changes or events (special cause), allowing for timely improvements and sustained quality. The control chart, a pivotal tool in SPC, visually displays data over time alongside a central line of upper and lower control...
129
 01:16
Estimating Population Mean with Known Standard Deviation
8.4K
To construct a confidence interval for a single unknown population mean μ, where the population standard deviation is known, we need sample mean as an estimate for μ and we need the margin of error. Here, the margin of error (EBM) is called the error bound for a population mean (abbreviated EBM). The sample mean is the point estimate of the unknown population mean μ.
The confidence interval estimate will have the form as follows:
(point estimate - error bound, point estimate +...
The confidence interval estimate will have the form as follows:
(point estimate - error bound, point estimate +...
8.4K