Related Experiment Video
Updated: Sep 29, 2026
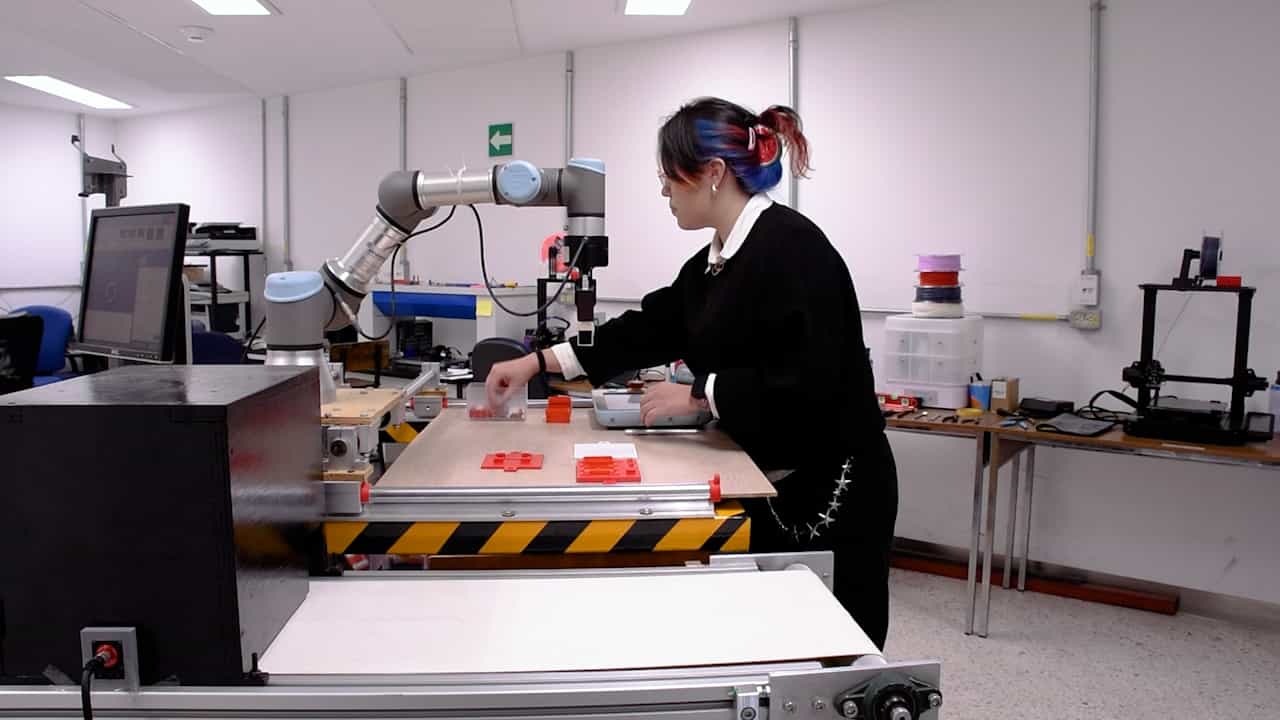
Simulation of a Scaled Assembly Process with Collaboration of a Robotic Arm and Monitoring through a Vision System for Quality Control
Published on: August 29, 2025
Internal quality control system for non-stationary, non-ergodic analytical processes based upon exponentially
Rob T P Jansen1, Mark Laeven, Wim Kardol
1Department of Clinical Chemistry, St Annaziekenhuis, Geldrop, The Netherlands. r.jansen@st-anna.nl

Abstract:
The analytical processes in clinical laboratories should be considered to be non-stationary, non-ergodic and probably non-stochastic processes. Both the process mean and the process standard deviation vary. The variation can be different at different levels of concentration. This behavior is shown in five examples of different analytical systems: alkaline phosphatase on the Hitachi 911 analyzer (Roche), vitamin B12 on the Access analyzer (Beckman), prothrombin time and activated partial thromboplastin time on the STA Compact analyzer (Roche) and PO2 on the ABL 520 analyzer (Radiometer). A model is proposed to assess the status of a process. An exponentially weighted moving average and standard deviation was used to estimate process mean and standard deviation. Process means were estimated overall and for each control level. The process standard deviation was estimated in terms of within-run standard deviation. Limits were defined in accordance with state of the art- or biological variance-derived cut-offs. The examples given are real, not simulated, data. Individual control sample results were normalized to a target value and target standard deviation. The normalized values were used in the exponentially weighted algorithm. The weighting factor was based on a process time constant, which was estimated from the period between two calibration or maintenance procedures. The proposed system was compared with Westgard rules. The Westgard rules perform well, despite the underlying presumption of ergodicity. This is mainly caused by the introduction of the starting rule of 12s, which proves essential to prevent a large number of rule violations. The probability of reporting a test result with an analytical error that exceeds the total allowable error was calculated for the proposed system as well as for the Westgard rules. The proposed method performed better. The proposed algorithm was implemented in a computer program running on computers to which the analyzers were linked on-line. Each result was evaluated on-line, and a limit violation was immediately reported. The system has performed satisfactorily in our laboratory for ten analyzers for over 1 year.
Related Concept Videos
 01:15
Introduction to Statistical Process Control
 01:05
Quality Control
Quality control helps track data, visualize trends, and identify variations, making it easier to detect deviations that may affect the accuracy of an analysis. One way to do this is by generating a quality control chart, which...
 00:58
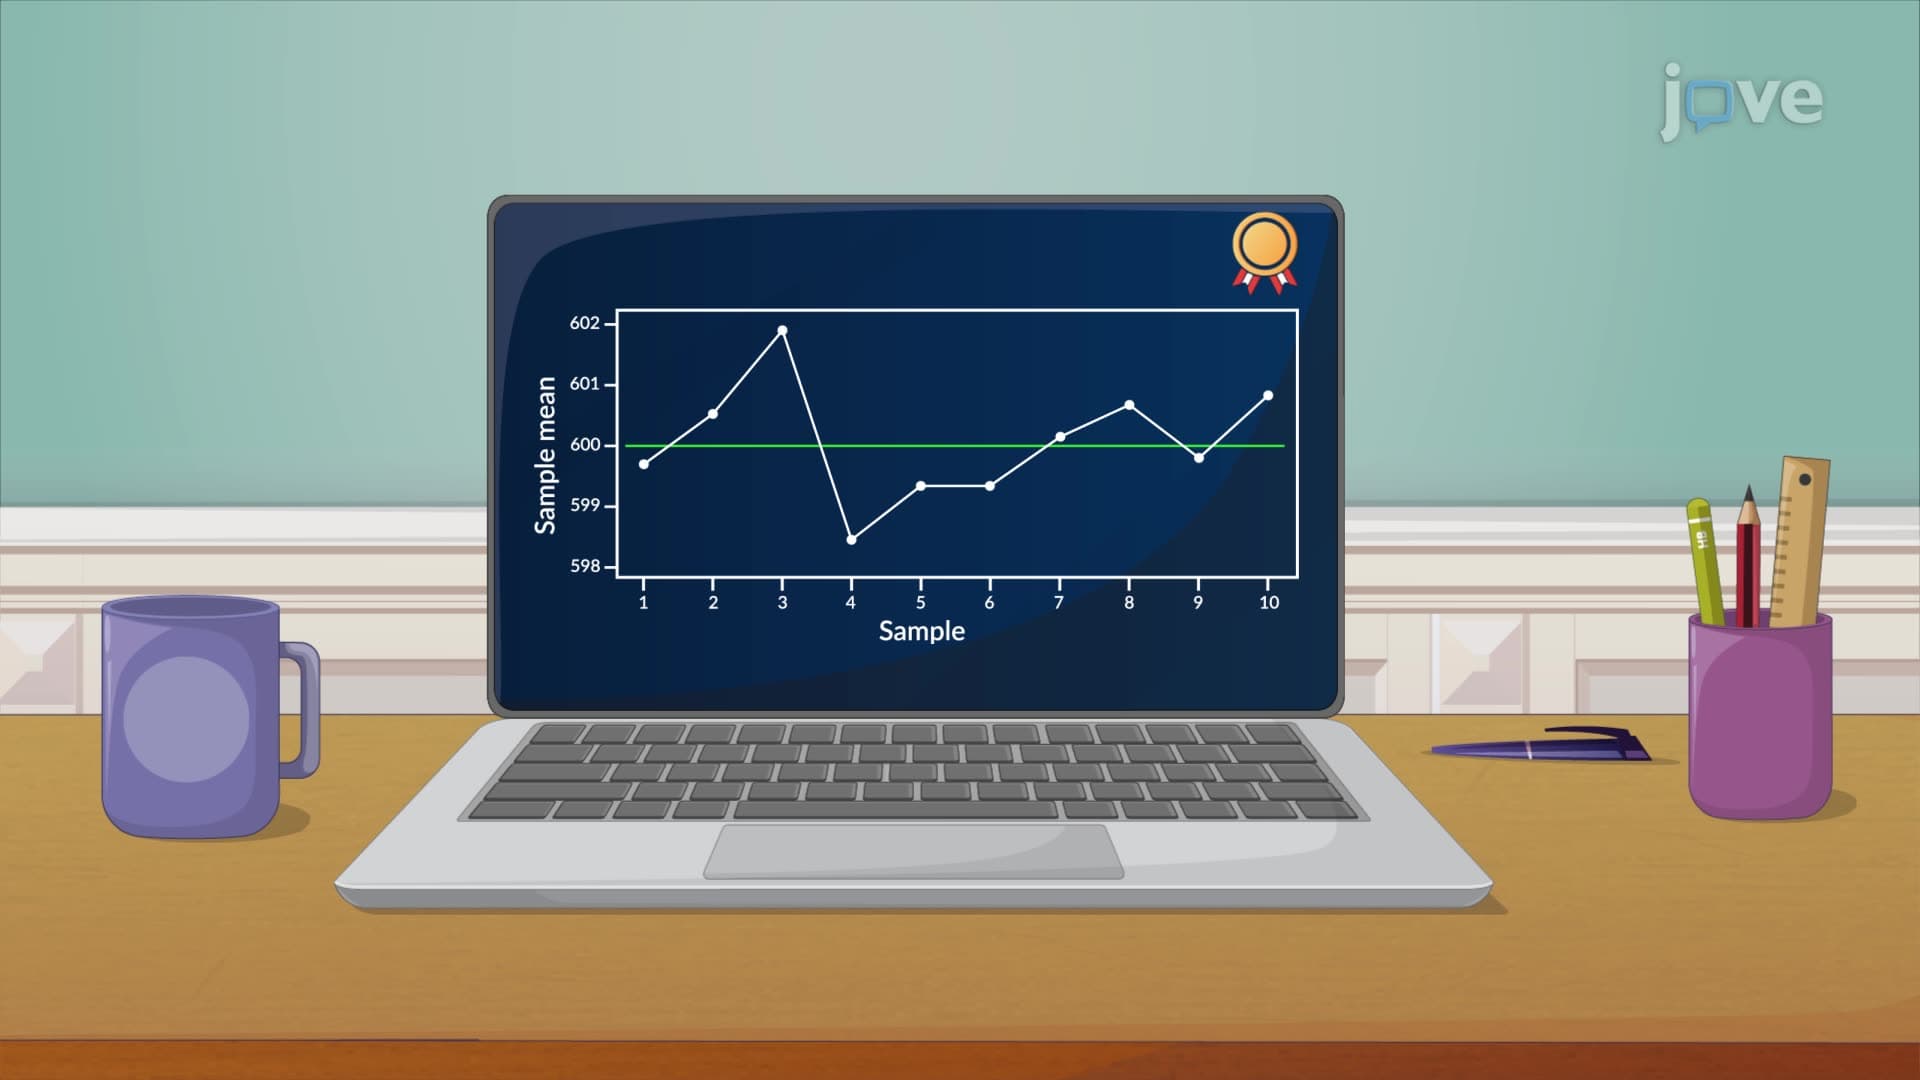
The X̄ Chart
The x̄ chart, often known as the individual control chart, is a crucial tool in statistical process control. It is designed to monitor process behavior and performance over time and is widely used in various industries to ensure that processes are operating at their optimum capacity and within specified limits.
A x̄ chart is constructed by plotting individual measurements of a quality characteristic in the order in which...
 01:13
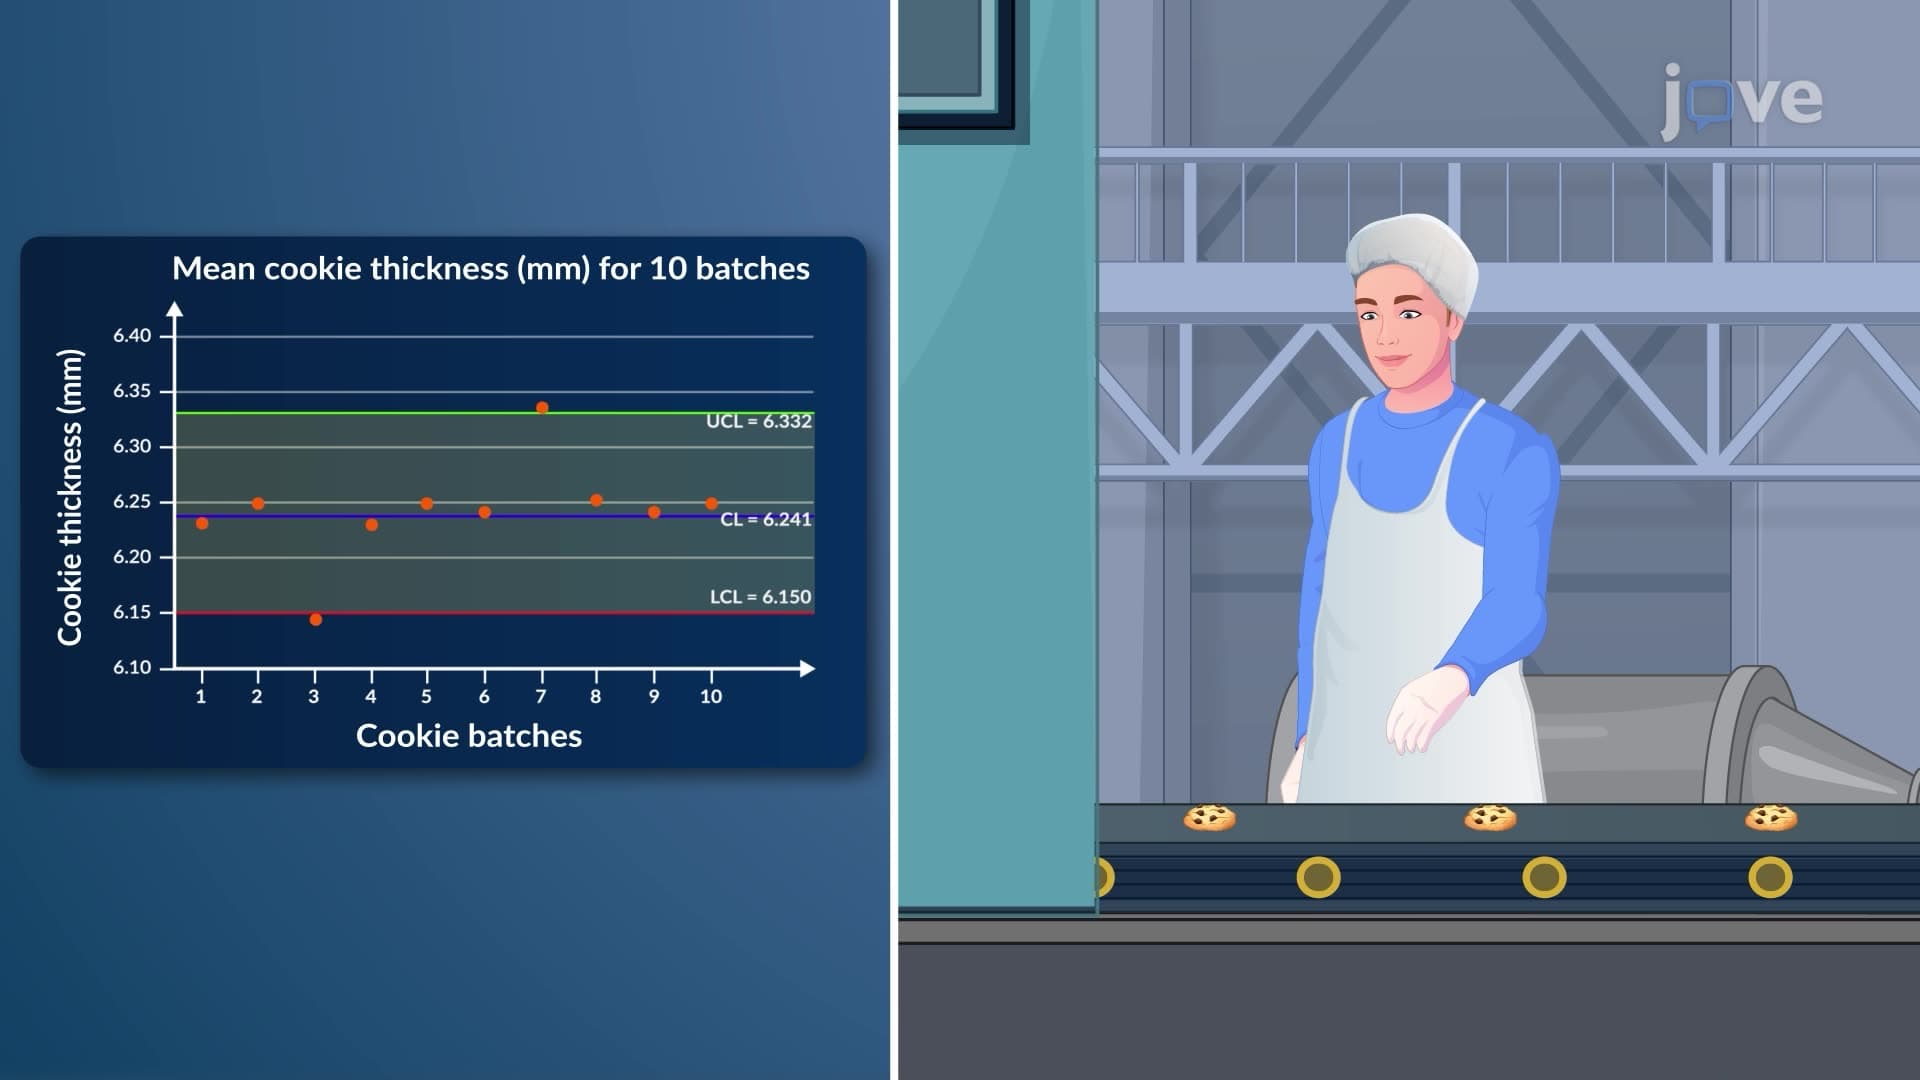
Interpreting X̄ Charts
An x̄ chart plots the values of individual measurements over time against control limits calculated from historical data. The central line represents the process mean,...
 01:19
Testing a Claim about Standard Deviation
The hypothesis testing for the claim of population standard deviation (or variance) requires the data and samples to be random and unbiased. The population distribution also must be normal. There is no specific requirement on the sample size as the estimation is based on the chi-square distribution.
As a first step, the hypothesis (null and alternative) concerning the claim about...
 01:10
Control Systems
At the heart...