Related Experiment Video
Updated: Jun 25, 2025

Surrogate Model Development for Digital Experiments in Welding
Published on: March 28, 2025
Effect of Process Parameters on Welding Residual Stress of 316L Stainless Steel Pipe
Xiaowei Jiang1, Wenhui Wang2, Chunguang Xu3
1School of Mechanical Engineering, Jiangsu University of Science and Technology, Zhenjiang 212003, China.

Abstract:
316L stainless steel pipes are widely used in the storage and transportation of low-temperature media due to their excellent low-temperature mechanical properties and corrosion resistance. However, due to their low thermal conductivity and large coefficient of linear expansion, they often lead to significant welding residual tensile stress and thermal cracks in the weld seam. This also poses many challenges for their secure and reliable applications. In order to effectively control the crack defects caused by stress concentration near the heat-affected zone of the weld, this paper establishes a thermal elastoplastic three-dimensional finite element (FE) model, constructs a welding heat source, and simulates and studies the influence of process parameters on the residual stress around the pipeline circumference and axial direction in the heat-affected zone. Comparison and verification were conducted using simulation and experimental methods, respectively, proving the rationality of the finite element model establishment. The axial and circumferential residual stress distribution obtained by the simulation method did not have an average deviation of more than 30 MPa from the numerical values obtained by the experimental method. This study also considers the effects of welding energy, welding speed, and welding start position on the pipe's circumferential and axial residual stress laws. The results indicate that changes in welding energy and welding speed have almost no effect on the longitudinal residual stress but have a more significant effect on the transverse residual stress. The maximum transverse residual stress is reached at a welding energy of 1007.4~859.3 J/mm and a welding speed of 6.6 mm/s. Various interlayer arc-striking deflection angles can impact the cyclic phase angle of the transverse residual stress distribution in the seam center, but they do not alter its cyclic pattern. They do influence the amplitude and distribution of the longitudinal residual stress along the circumference. The residual stress distribution on the surface of the pipe fitting is homogenized and improved at 120°.
More Related Videos
Related Concept Videos
 01:26
Residual Stresses
 01:09
Bending of Material: Problem Solving
 01:23
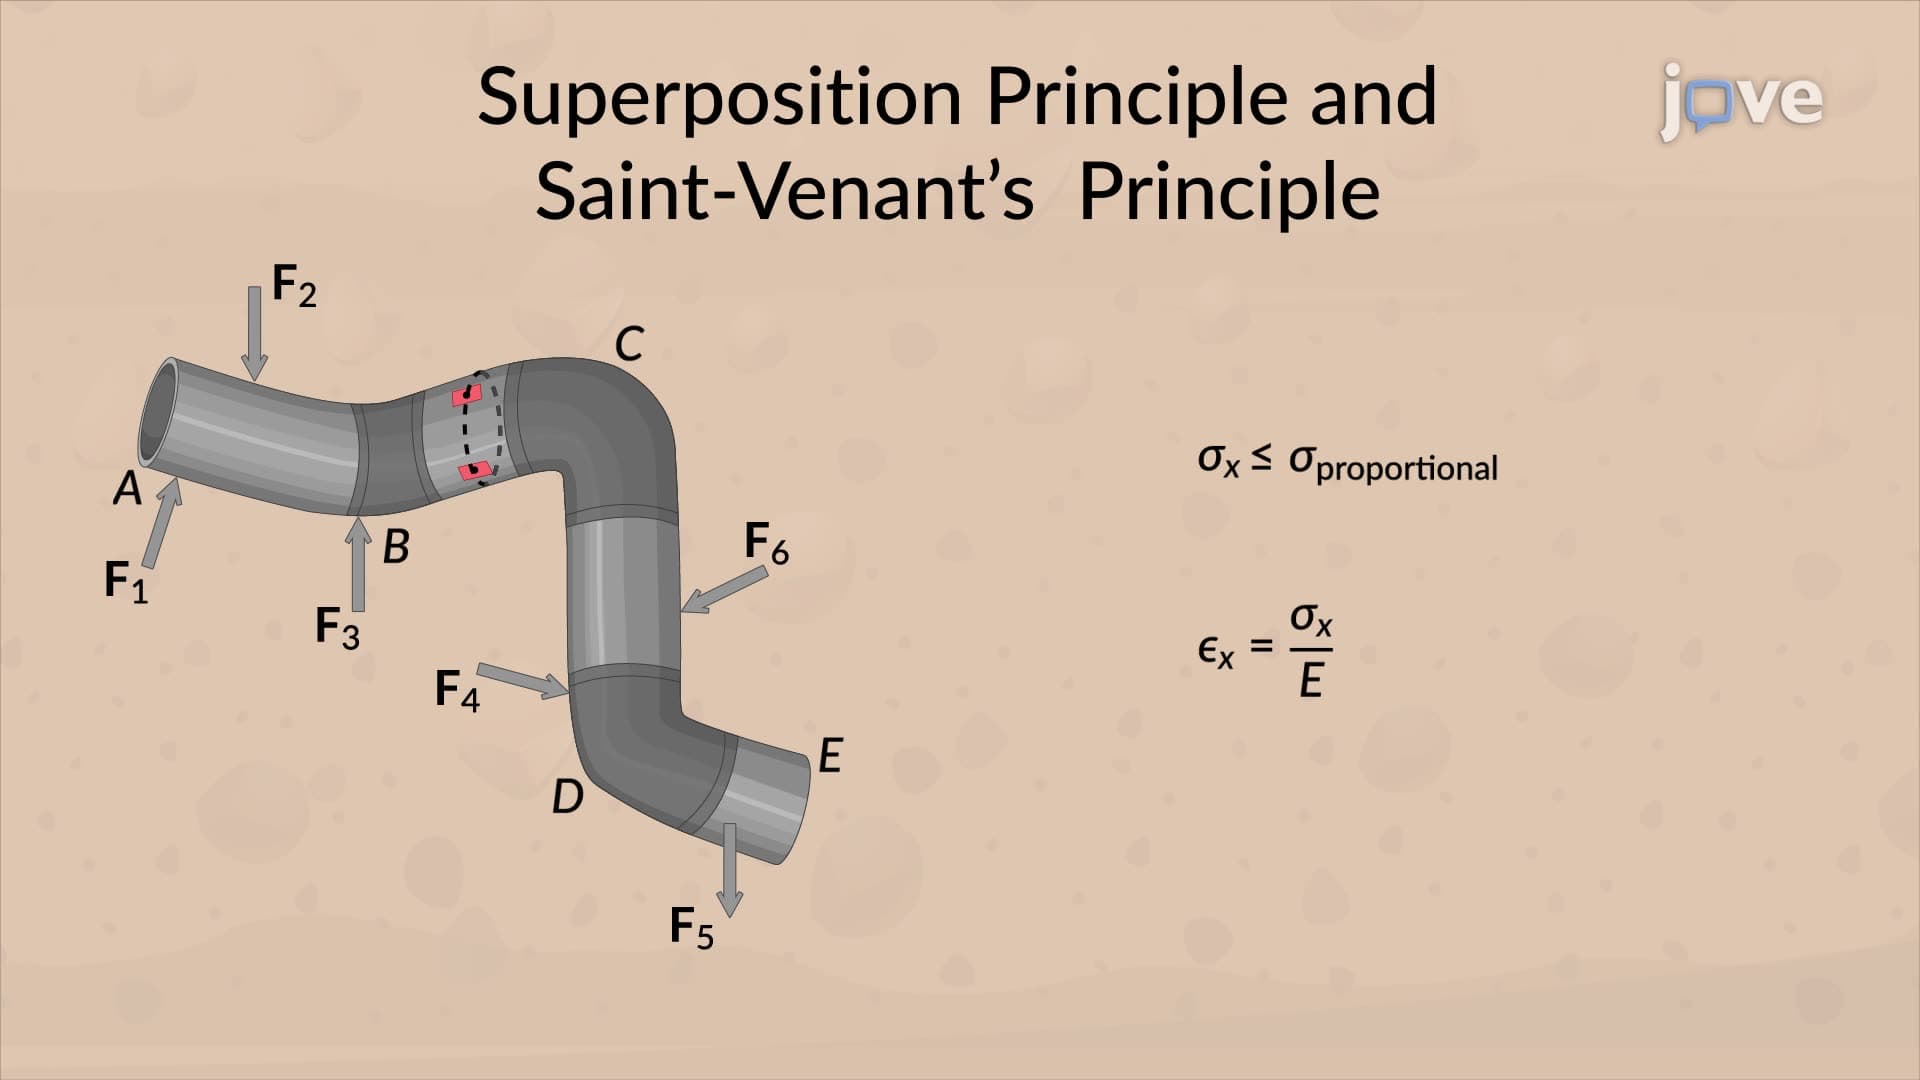
Stresses under Combined Loadings
The process begins by slicing the tube at critical points and analyzing the internal forces and stress components at these sections, focusing on the centroid. Normal stresses, generated by axial forces and bending moments, are either compressive or tensile and vary across the section from...
 01:24
Stress Concentrations
 01:10
Residual Stresses in Circular Shafts
 01:12
Temperature Dependent Deformation