Related Experiment Video
Updated: Jan 13, 2026

Ultrasonic Fatigue Testing in the Tension-Compression Mode
Published on: March 7, 2018
Study on the Fatigue Bending Strength of Cylindrical Components Manufactured by External WAAM
Van-Minh Nguyen1, Pham Son Minh1, Dang Thu Thi Phan1
1Faculty of Mechanical Engineering, HCMC University of Technology and Education, Ho Chi Minh City 71307, Vietnam.

Abstract:
This study investigates the fatigue bending strength, measured as the Mean of Fatigue Cycles (N), of cylindrical components produced by external wire arc additive manufacturing (WAAM) through a Taguchi L25 orthogonal array and linear regression analysis. Five welding parameters-welding current (Ampe), offset distance (mm), step length (mm), welding speed (mm/min), and specimen gauge diameter (mm)-were evaluated to maximize N using signal-to-noise (S/N) ratios. Nominal bending stresses (σ) ranged from 45 to 54 MPa, ANOVA on raw replicate data (25 runs, 3 replicates) confirmed specimen gauge diameter = 17 mm and weld current = 125 A as dominant, with F = 171.62 (p < 0.001, eta2 = 0.62 [95% confidence intervals (CI) 0.55-0.68]) for specimen gauge diameter and F = 6.13 (p < 0.001, eta2 = 0.13 [95% CI 0.08-0.18]) for weld current, accounting for ~75% of the variance. Optimal settings (offset distance = 3.0 mm, step length = 1000 mm, welding speed = 550 mm/min, specimen gauge diameter = 17 mm) achieved S/N = 111.35 dB, predicting N ≈ 350,000-380,000 cycles, a 22-33% improvement. Interactions between specimen gauge diameter and speed, and between weld current and offset distance, suggested enhanced strength at speed = 400-450 mm/min for specimen gauge diameter = 17 mm. Basquin's law (b ≈ 0.72, R2 = 0.992) confirmed weld current as key. The linear regression model (adjusted R2 = 0.9506) had coefficients for specimen gauge diameter (+70,120 cycles/mm, p < 0.001) and weld current (+1088 cycles/Ampe, p = 0.02), but lower test R2 = 0.7212 via cross-validation (60/20/20 split) indicates overfitting due to small dataset size (25 runs), suggesting larger datasets or nonlinear models (e.g., polynomial regression, RSM). Confirmation runs (N = 317,082, 95% CI [287,000-347,000]) validated the results within ~13% error. WAAM reaches 80-90% of traditional manufacturing (TM) fatigue performance, with a 10-20% gap due to the microstructure; recommendations include post-treatments and safety factors (~1.2).
Related Concept Videos
 01:21
Fatigue
 01:09
Bending of Material: Problem Solving
 01:11
Bending of Members Made of Several Materials
Hooke's Law determines stress in each material, stating that stress is proportional to strain but varies due to each material's...
 01:23
Design of Prismatic Beams for Bending
 01:10
Bending
In pure bending, the bending stress in a beam is calculated based on the bending moment and...
 01:23
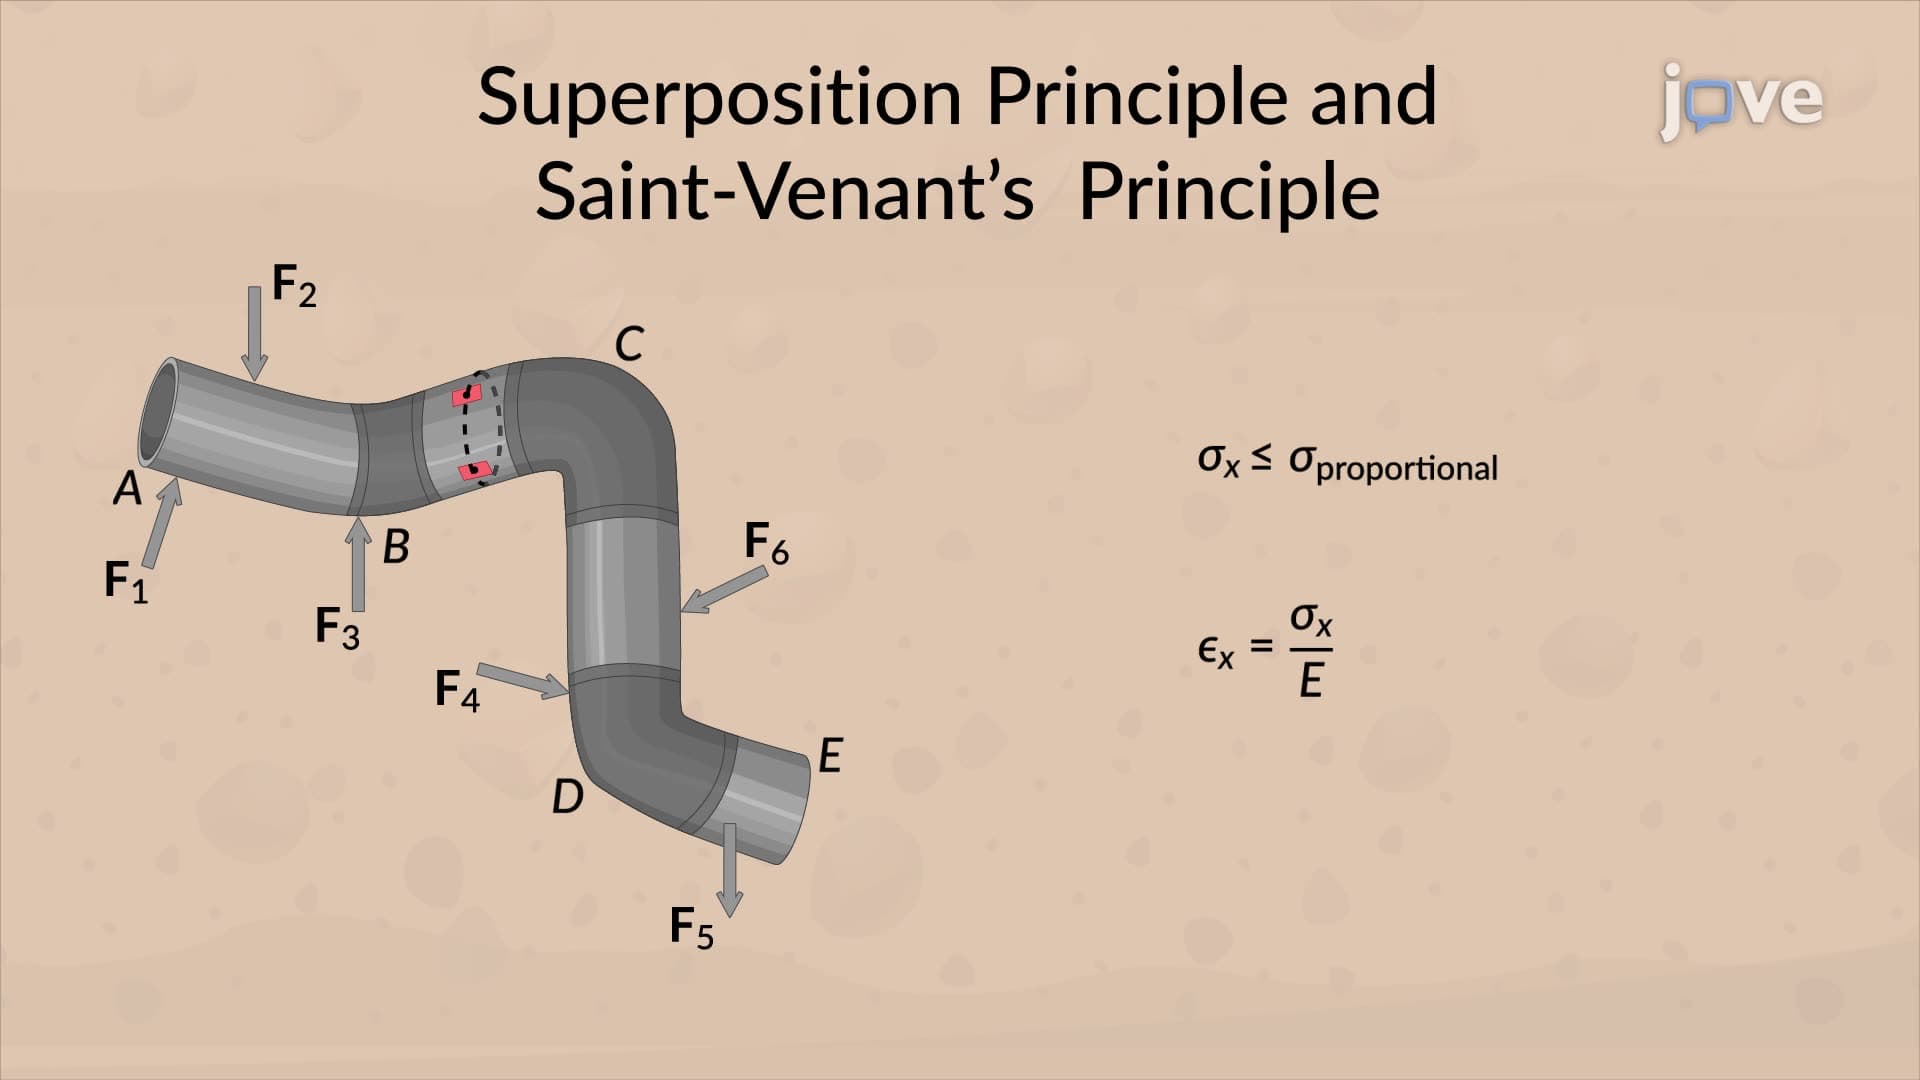
Stresses under Combined Loadings
The process begins by slicing the tube at critical points and analyzing the internal forces and stress components at these sections, focusing on the centroid. Normal stresses, generated by axial forces and bending moments, are either compressive or tensile and vary across the section from...