Related Experiment Video
Updated: Jan 6, 2026

A Soft Tooling Process Chain for Injection Molding of a 3D Component with Micro Pillars
Published on: August 4, 2018
Applying a new mold temperature control strategy to improve the tensile strength of thin wall products in injection
Thanh Trung Do1, Duc Thuan Huynh2,3,4, Tran Anh Son2,3
1Ho Chi Minh City University of Technology and Education (HCMUTE), Ho Chi Minh City, Vietnam.

Abstract:
Mold temperature control critically influences injection molding, impacting product quality and production efficiency. High mold temperatures enhance surface quality but prolong cooling, increasing cycle time, whereas low temperatures cause defects like weak weld lines and incomplete filling. This study aims to reduce cycle time and enhance tensile strength of thin-wall injection-molded products by developing an innovative mold temperature control strategy using induction heating to preheat mold inserts. The primary objective is to eliminate in-cycle heating delays while ensuring optimal mold temperatures for improved mechanical properties. However, the power consumption of this process significantly increases due to the energy-intensive nature of induction heating. Research involved numerical simulations and experimental validation. COMSOL Multiphysics analyzed thermal and electromagnetic interactions, modeling temperature distributions for heating distances (G = 5, 10, 15 mm) and times (1-8 s). Moldex3D simulated polymer flow behavior, assessing filling capabilities for materials (PC, ABS, PA6, PP). Experiments employed the external induction heating with rotational structure for mold temperature control system (Ex-IHRS), featuring a rotational mechanism to swap preheated inserts, with real-time temperature measurements via sensors and infrared cameras at points S1, S2, and S3. Tensile strength tests evaluated mechanical performance. Rapid heating within 5-8 s maintained stable mold temperatures without extending cycle time, outperforming traditional methods like resistance or steam heating. Significant tensile strength improvements occurred, with PC increasing from 111.9 MPa to 123 MPa after 6 s of heating, ABS reaching 91.3 MPa after 4 s, PA6 rising from 55.4 MPa to 62.8 MPa, and PP improving from 41.3 MPa to 47.3 MPa. Enhanced weld line integrity and reduced frozen layers drove these gains, minimizing defects in thin-wall components. Simulations showed less than 5% deviation from experimental data, validating the approach's accuracy. Despite higher power consumption, this induction heating strategy optimizes production efficiency and enhances product quality, offering a promising advancement for thin-wall and microinjection molding applications.
More Related Videos
Related Concept Videos
 01:23
Physical Methods for Controlling Microbial Growth: Temperature
 01:25
Yield Criteria for Ductile Materials under Plane Stress
The Maximum Shearing Stress Criterion, also known as...
 01:26
Residual Stresses
 01:15
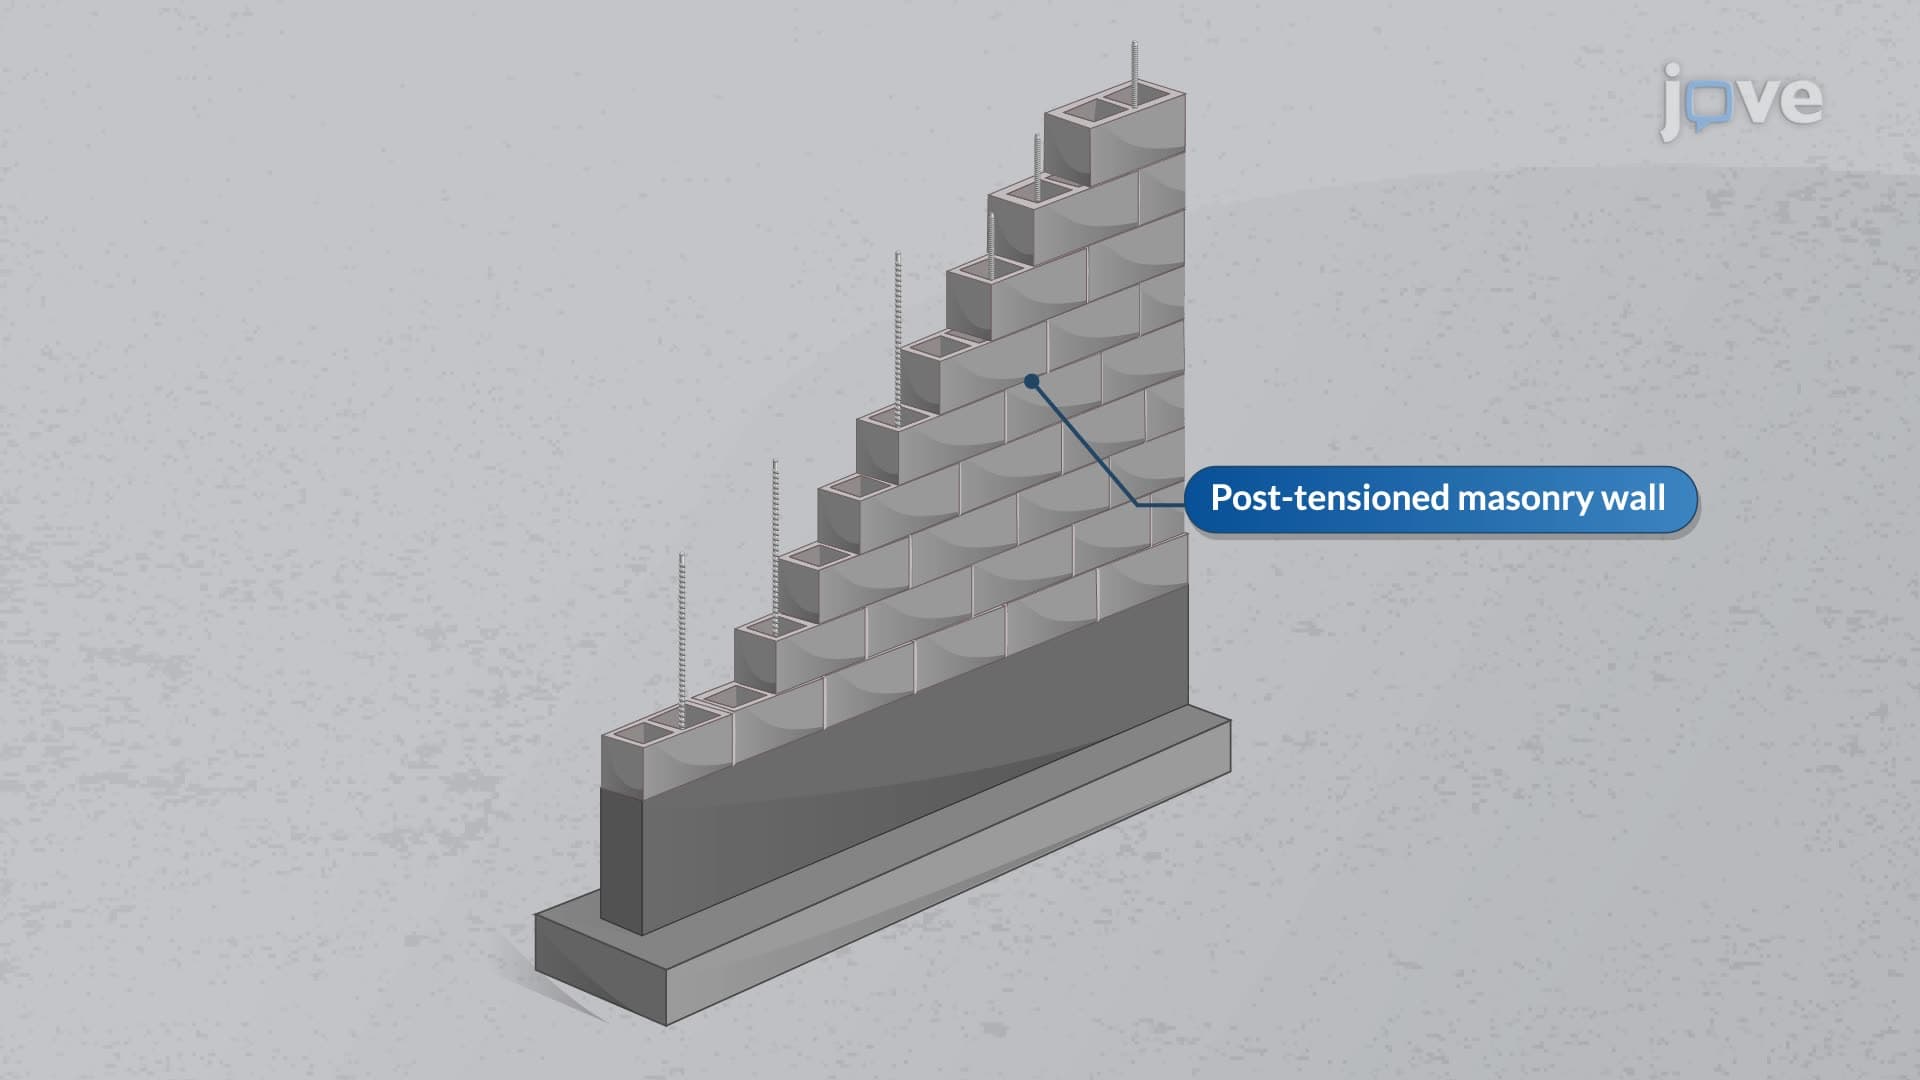
Posttensioned Masonry Walls
Post-tensioned masonry walls use high-strength steel rods or flexible tendons to enhance the strength and efficiency of masonry structures. These elements are securely anchored to the foundation and extend vertically either within the cores of the masonry units or between the masonry wythes. The construction process involves building the wall with these tensioning elements in place and allowing the mortar to fully cure.
Following the curing process, the tensioning begins. Steel rods are...
 01:19
Thermal Strain