Related Experiment Video
Updated: Nov 20, 2025

Automatic Laser-based Geometry Capture for Finite Element Analysis of Weld Beads
Published on: July 25, 2025
Advanced Structural and Technological Method of Reducing Distortion in Thin-Walled Welded Structures
Piotr Horajski1, Lukasz Bohdal1, Leon Kukielka1
1Faculty of Mechanical Engineering, Koszalin University of Technology, 75-620 Koszalin, Poland.

Abstract:
The article presents an innovative method of reducing welding distortions of thin-walled structures by introducing structural and technological changes. The accuracy of the method was demonstrated on the example of welding the stub pipes to the outer surface of a thin-walled tank with large dimensions, made of steel 1.4301 with a wall thickness of 1.5 × 10⁻³ (m). During traditional Gas Tungsten Arc Welding (GTAW), distortions of the base are formed, the flatness deviation of which was 11.9 × 10⁻³ (m) and exceeded the permissible standards. As a result of structural and technological changes, not only does the joint stiffness increase, but also a favorable stress state is introduced in the flange, which reduces the local welding stresses. Numerical models were developed using the finite element method (FEM), which were used to analyze the residual stresses and strains pre-welding, in extruded flanges, in transient, and post-welding. The results of the calculations for various flanges heights show that there is a limit height h = 9.2 × 10⁻³ (m), above which flange cracks during extrusion. A function for calculating the flange height was developed due to the required stress state. The results of numerical calculations were verified experimentally on a designed and built test stand for extrusion the flange. The results of experimental research confirmed the results of numerical simulations. For further tests, bases with a flange h = 6 × 10⁻³ (m) were used, to which a stub pipe was welded using the GTAW method. After the welding process, the distortion of the base was measured with the ATOS III scanner (GOM a Zeiss company, Oberkochen, Germany). It has been shown that the developed methodology is correct, and the introduced structural and technological changes result in a favorable reduction of welding stresses and a reduction in the flatness deviation of the base in the welded joint to 0.39 × 10⁻³ (m), which meets the requirements of the standards.
Related Concept Videos
 01:17
Steel Fastening Techniques
Rivets are cylindrical steel fasteners with a specially designed head. During application, rivets are heated until white-hot and then inserted through pre-drilled holes in the steel sections. A pneumatic hammer is used to shape the exposed end into a second head, securing the sections together.
Bolting is another...
 01:23
Unsymmetric Loading of Thin-Walled Members
The concept of the shear center is crucial in countering the...
 01:24
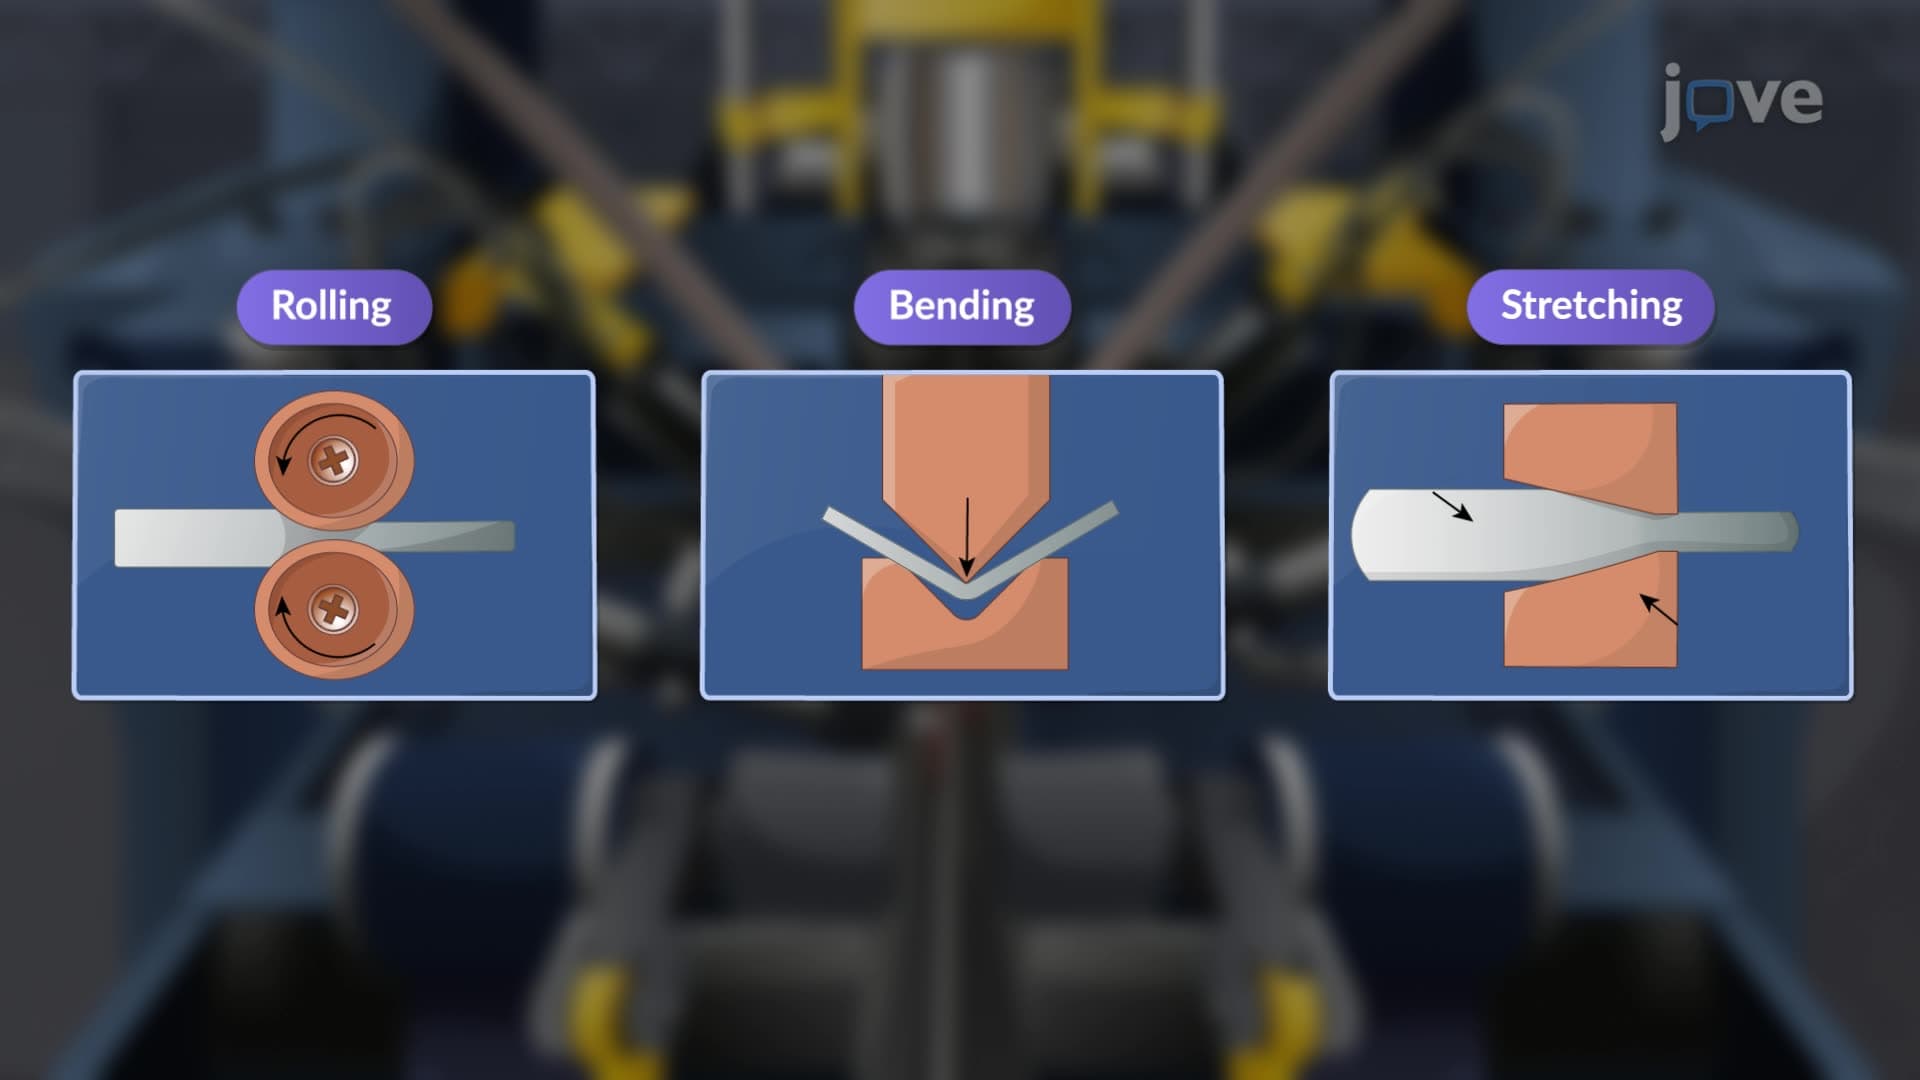
Structural Steel Products
Once shaped, the steel's final form emerges as a continuous length, which is then segmented by a hot saw into manageable pieces. These segments...
 01:15
Thin-Walled Hollow Shafts
 01:07
Unsymmetric Loading of Thin-Walled Members: Problem Solving
To compute the shear forces, find the shear flow at a specific distance from the endpoint using the vertical shear and the moment of inertia values. The total shear force on the flange is calculated by integrating the shear flow from one end of the flange to the other.
Next, calculate the moments of...
 01:26
Residual Stresses